Each silhouette utilizes tubular circular knitting technology that integrates localized compression, sweat ventilation micro-mesh, and multi-directional flex directly into the garment matrix.
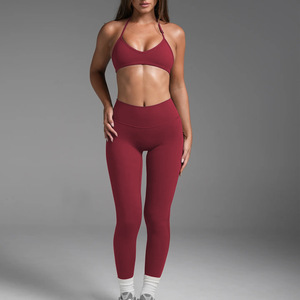
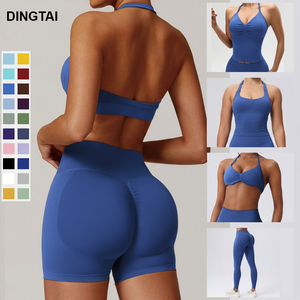
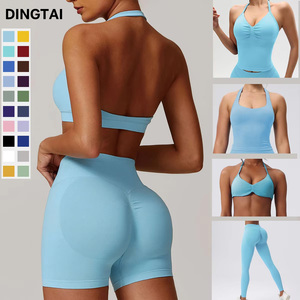
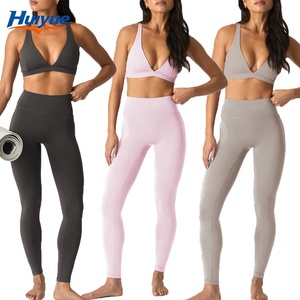
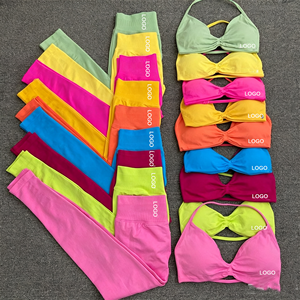
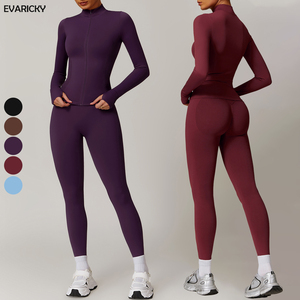
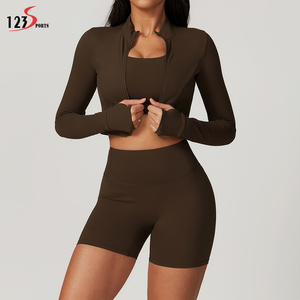
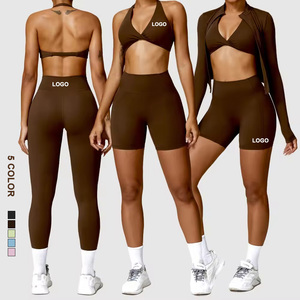
Designing and manufacturing seamless performance wear for the Mumbai metropolitan region requires solving distinct physical and lifestyle wear characteristics that conventional cut-and-sew apparel cannot satisfy.
Mumbai's coastal ambient humidity consistently exceeds 75% to 85% for eight months annually. Conventional flatlocked cotton or low-grade polyester retains cutaneous sweat, causing thermal distress and abrasive chafing. Our circular seamless construction uses Polyamide 6.6 with cross-sectional hydrophilic capillary microchannels, expelling sweat directly into ambient air for lightning-fast dry times during high-heat tropical workouts.
Due to moisture entrapment inherent to Mumbai's dense urban monsoon season, garments are treated with eco-certified silver-ion or organic antimicrobial finishing agents. This molecular-level coating halts bacterial reproduction (Staphylococcus aureus and Klebsiella pneumoniae), completely mitigating locker-bag odor accumulation for city commuters moving between offices and fitness hubs.
Elite training centers across Bandra West, Lower Parel, and Juhu focus on Pilates reformers, anti-gravity aerial yoga, and high-cadence spin classes. Athletes demand high-waist compressive ribbing that remains 100% squat-proof under intense halogen lighting without rolling down, digging into abdominal walls, or generating irritating seam impressions on skin.
Mumbai's celebrity wellness culture and entertainment ecosystem have normalized activewear as daily streetwear across Bandra's cafes and corporate co-working lounges in the Bandra Kurla Complex (BKC). Our garments blend matte dope-dyed yarns and minimalist structural ribs that transition effortlessly from power workouts to high-street social engagements.
A macroeconomic and textile-engineering analysis of the shift from traditional cut-and-sew garments to seamless circular knitting in the Western Indian athletic market.
The Indian activewear sector has experienced unprecedented compound annual growth rates (CAGR exceeding 18.5%), centered directly in urban epicenters like Mumbai, Delhi-NCR, and Bengaluru. Emerging direct-to-consumer athletic brands are dismantling traditional distributor layers by launching high-margin, digital-first product lines.
However, modern digital shoppers in Mumbai demonstrate rapid product return behaviors if leggings display shear opacity flaws (becoming see-through during squats) or suffer chafing failures. Brand longevity hinges entirely on factory-floor technical mastery: needle precision, tension uniformity, and elastane recovery resilience that guarantees zero fabric degradation over 50+ industrial wash cycles.
For brands operating throughout Maharashtra, supply-chain velocity is decisive. Our export facilities coordinate directly with Jawaharlal Nehru Port Trust (JNPT / Nhava Sheva) ocean freight routes and Mumbai Air Cargo (BOM). This direct connectivity provides low transit lead times compared to inland competitors.
By streamlining customs clearance documentation under exact Harmonized System (HS) codes (such as Chapter 61 for knitted and crocheted athletic wear), domestic brands bypass intermediate storage bottlenecks, reducing total freight handling costs and landing fresh product lines precisely ahead of festive and seasonal demand surges.
| Performance Characteristic | Our Circular Seamless Knitting (Santoni Top2V) | Conventional Cut-and-Sew (Local Garment Assembly) |
|---|---|---|
| Structural Seams | Zero Side Seams (Continuous single tubular body) | Heavy side, hip, and underarm overlock stitching |
| Fabric Scrap & Material Waste | < 3.5% Waste (Knitted directly to exact perimeter) | 18% – 25% waste from cutting flat fabric markers |
| Compression Control | Digitally programmed variable stitch tension (Needle-level) | Relies entirely on cutting panels smaller and sewing tight elastic |
| Skin Irritation Index | Ultra-smooth interior surface; zero skin friction points | Bulk thread points cause pressure necrosis & sweat chafing |
| Burst Strength & Elastic Recovery | Up to 98.4% shape retention after 20,000 extension cycles | Seam breakage and thread pops at high-stress joint areas |
Combining world-class circular knitting technology with bespoke OEM/ODM private-label capabilities, we empower international and domestic activewear labels to deliver uncompromised quality.
Our manufacturing floor houses 20 original Santoni Top2V 28-gauge circular knitting machines. We do not broker or outsource our knitting. By retaining 100% in-house machinery operation, we achieve exact loop control, eliminating irregular barre marks and yarn-slip defects across bulk runs.
Transforming CAD sketches or reference garments into digital machine stitch programs occurs on our production floor. Samples are knitted, dyed, and shipped for fit review within 5 to 7 days, shaving months off standard Asian apparel development timelines.
To support high-growth labels testing new collection palettes, our baseline production tier begins at 1,000 pieces per style, which can be distributed across up to 2 size tiers and 3 bespoke Pantone colorways (e.g., 500 Size M and 500 Size L split across preferred shades).
We source raw micro-denier Nylon 6.6 and recycled polyamide alongside high-recovery Spandex. Partner dye mills run precision pressure vessel dyeing, ensuring ΔE color variance below 0.5 against client spectrophotometer digital standards under both D65 daylight and store LED lighting.
Every knitted tube is hand-inspected under illuminated inspection tables prior to heat setting. Finished garments undergo 4-point stretching tests, seam burst assessments on gusset bars, and rub fastness evaluations before being packaged in retail-ready branded biodegradable polybags.
Shipping to 25+ countries worldwide, we maintain dedicated export logistics desks. Indian brand partners benefit from direct ocean bills of lading to Nhava Sheva (JNPT) or priority air cargo into Chhatrapati Shivaji Maharaj International Airport (BOM), ensuring frictionless documentation.
Direct answers for athletic apparel brand founders, corporate procurement managers, and apparel retail merchandisers navigating overseas manufacturing and local fulfillment.
We are a 100% direct manufacturer operating our own circular knitting production facility. We configure raw micro-filament yarns, program machine coding on 20 Santoni Top2V machines, manage wet-finishing and heat setting with accredited dye houses, and run our own finishing, tagging, and packing lines. You communicate directly with factory engineers, eliminating intermediary margins and ensuring complete production transparency.
We supply complete export documentation sets including Commercial Invoices, Detailed Packing Lists, Certificates of Origin, and Sea Waybills/Air Waybills coded under accurate HSN Chapter 61 tariffs. Shipments bound for the Mumbai market can land via ocean freight at Nhava Sheva Port (JNPT) for maximum cost efficiency on container-load volumes, or arrive via Chhatrapati Shivaji Maharaj International Airport Cargo Complex (BOM) within days for time-critical capsule drops.
Our baseline production runs require 1,000 pieces per style. Within that 1,000-piece commitment, we provide flexibility for emerging brand scaling: you can divide the quantity across up to 2 size dimensions (e.g., Small/Medium and Large/X-Large) and split across up to 3 custom colorways (e.g., 400 Black, 300 Slate Blue, 300 Terracotta). Bespoke repeat orders for established brands are scalable up to 100,000+ pieces monthly.
Sheer fabric failure (becoming translucent during bending or stretching) occurs when manufacturers thin out gauge counts to save yarn weight. We utilize tight 28-gauge circular knitting cylinders that weave dense, double-knit elastane interlacing loops. Our garments undergo rigorous digital lightbox elongation testing and two-way elongation stretch tests, guaranteeing 100% opacity, anti-microbial resilience, and squat-proof wear even under extreme high-sweat coastal fitness conditions.
Yes. Many brand clients supply physical reference garments, 3D digital mockups, or simple design tech-packs. Our in-house technical programming team translates these designs into Santoni matrix files, engineering targeted contour lines, under-bust support bands, and laser-mapped ventilation channels. We provide custom heat-sealed inner collar transfer logos, branded woven drawstrings, and custom retail packaging tailored to your brand identity.
Once your technical profile, yarn selection, and Pantone color specifications are confirmed, physical proto-samples are typically knitted, assembled, and dispatched within 5 to 7 business days via express air courier (DHL/FedEx). This enables your merchandising team in Mumbai to evaluate compression stretch, hand-feel, and seam placement rapidly before authorizing bulk circular machine runs.
Consult directly with our textile engineers and global export managers. Receive custom yarn specifications, rapid sample schedules, and comprehensive DDP / CIF Nhava Sheva pricing for your brand's next activewear launch.