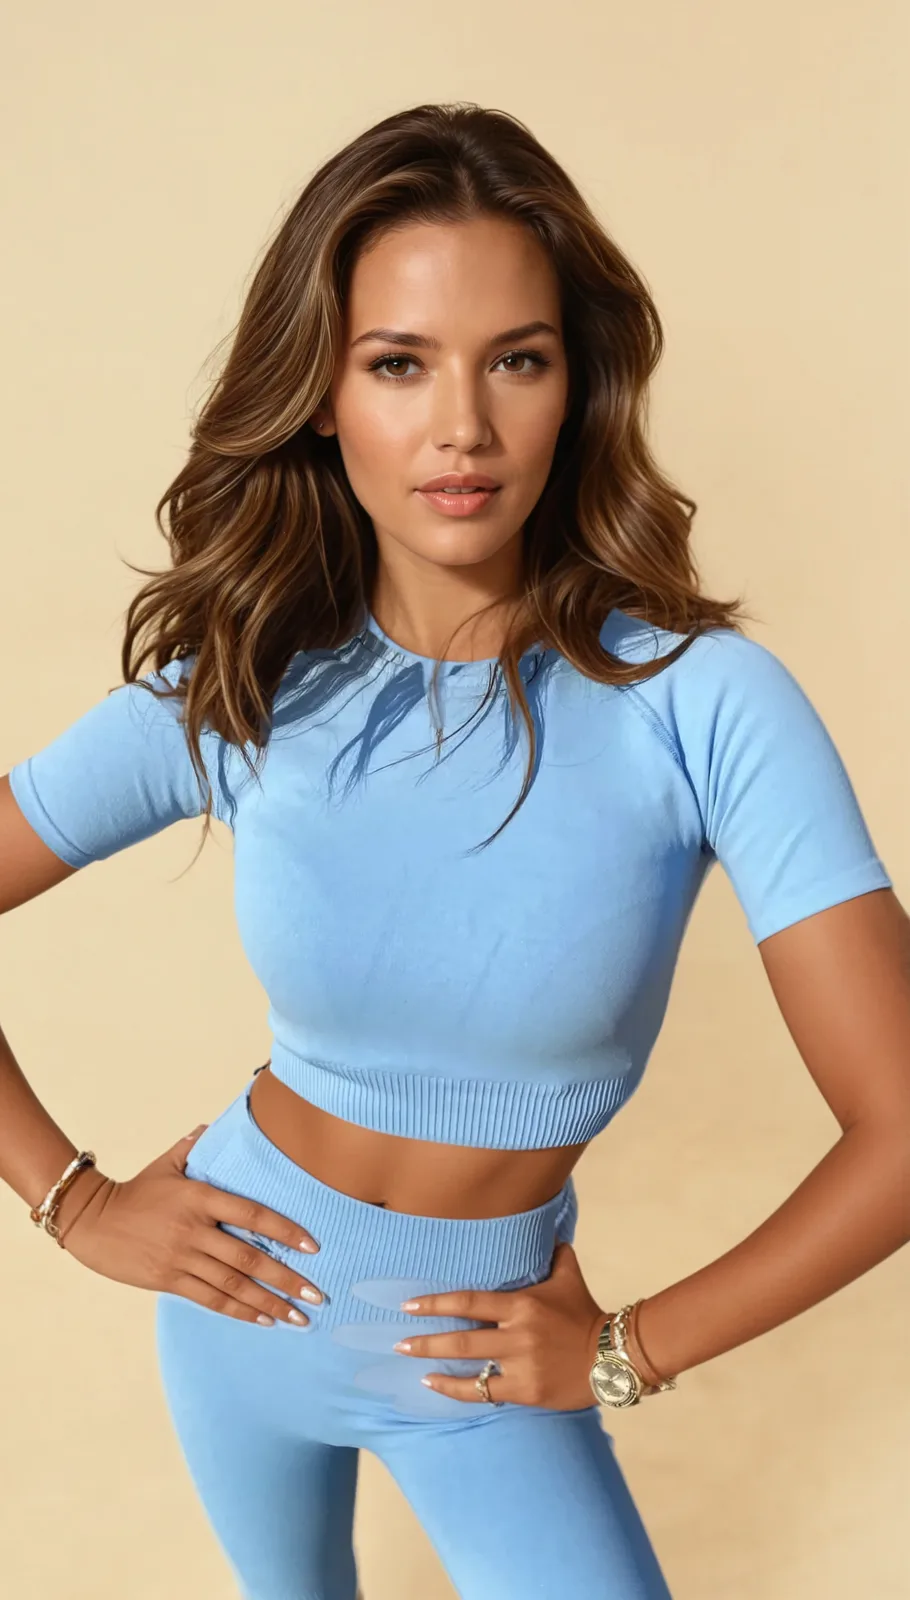
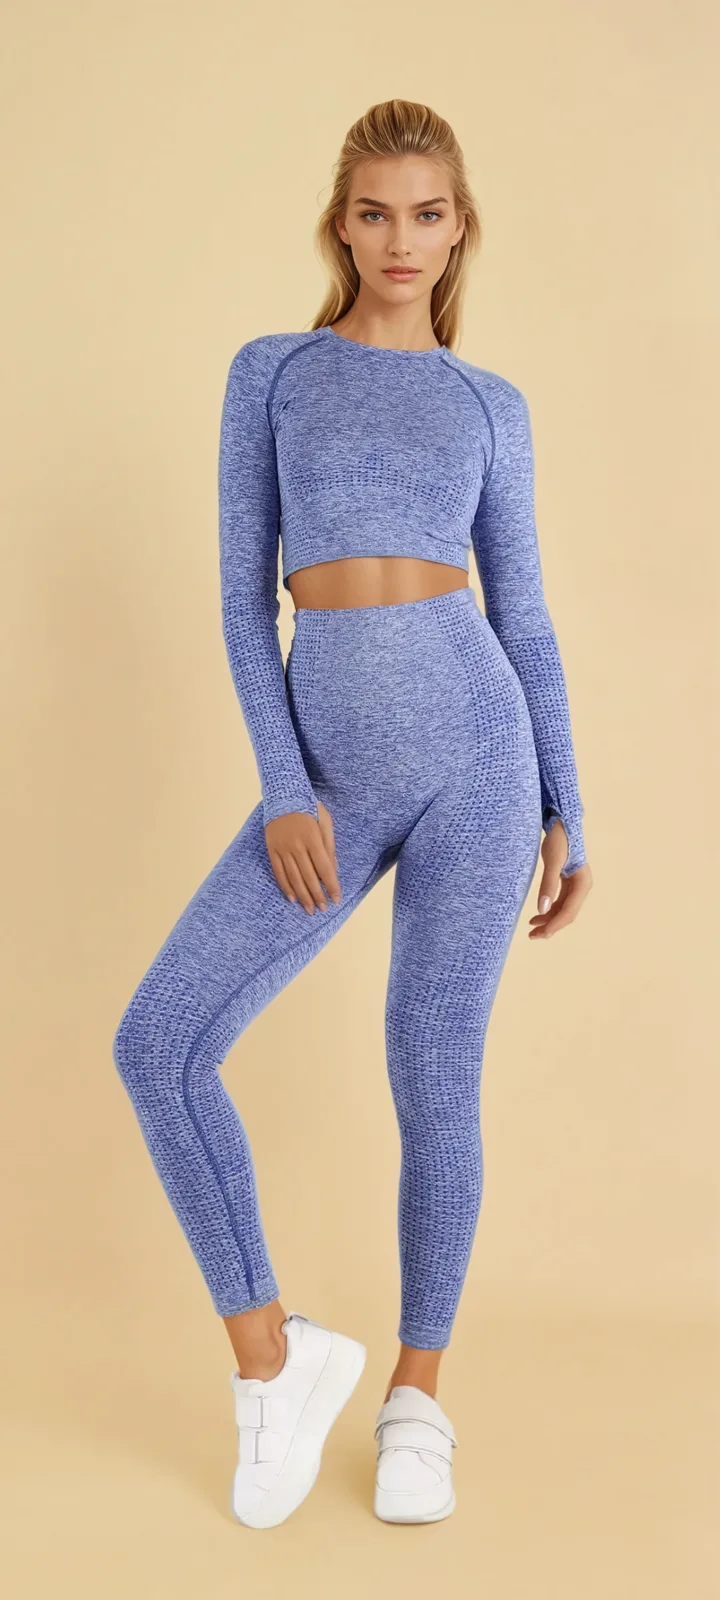
Constructed with zoned micro-ribbing down the lateral thighs and lateral torso. Uses high-modulus air-jet covered Lycra with air-textured Polyamide 6.6 to sculpt without pinching or rolling at the waistband.
Get Tech Pack & Spec Sheet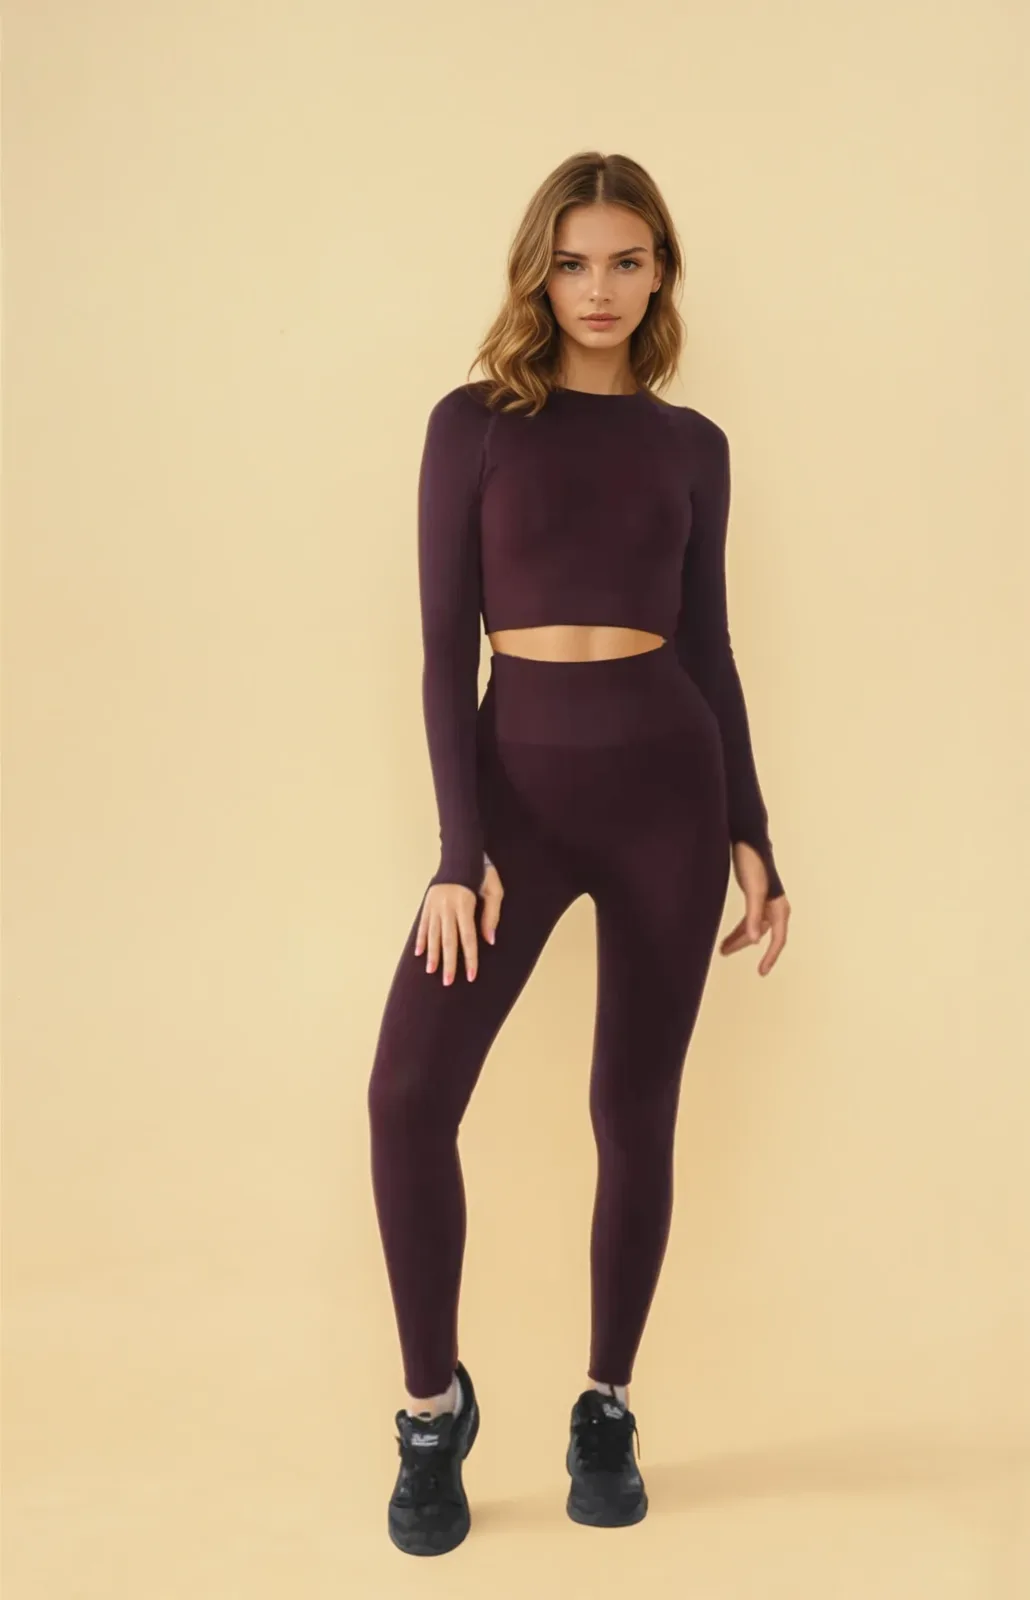
B2B Sourcing Authority · İstanbul, Türkiye
Since 2019, Overfit Seamless has operated as a specialized circular knitting factory in Beylikdüzü, İstanbul. We engineer custom seamless workout sets for high-growth athletic apparel labels across North America and Europe. By deploying 20 in-house Santoni Top2V machines (gauge 28), we eliminate unnecessary middleman margins, resolve common color mismatches between bra and leggings, and deliver verified production-grade samples in just 5 to 7 business days.
Core Product Engineering
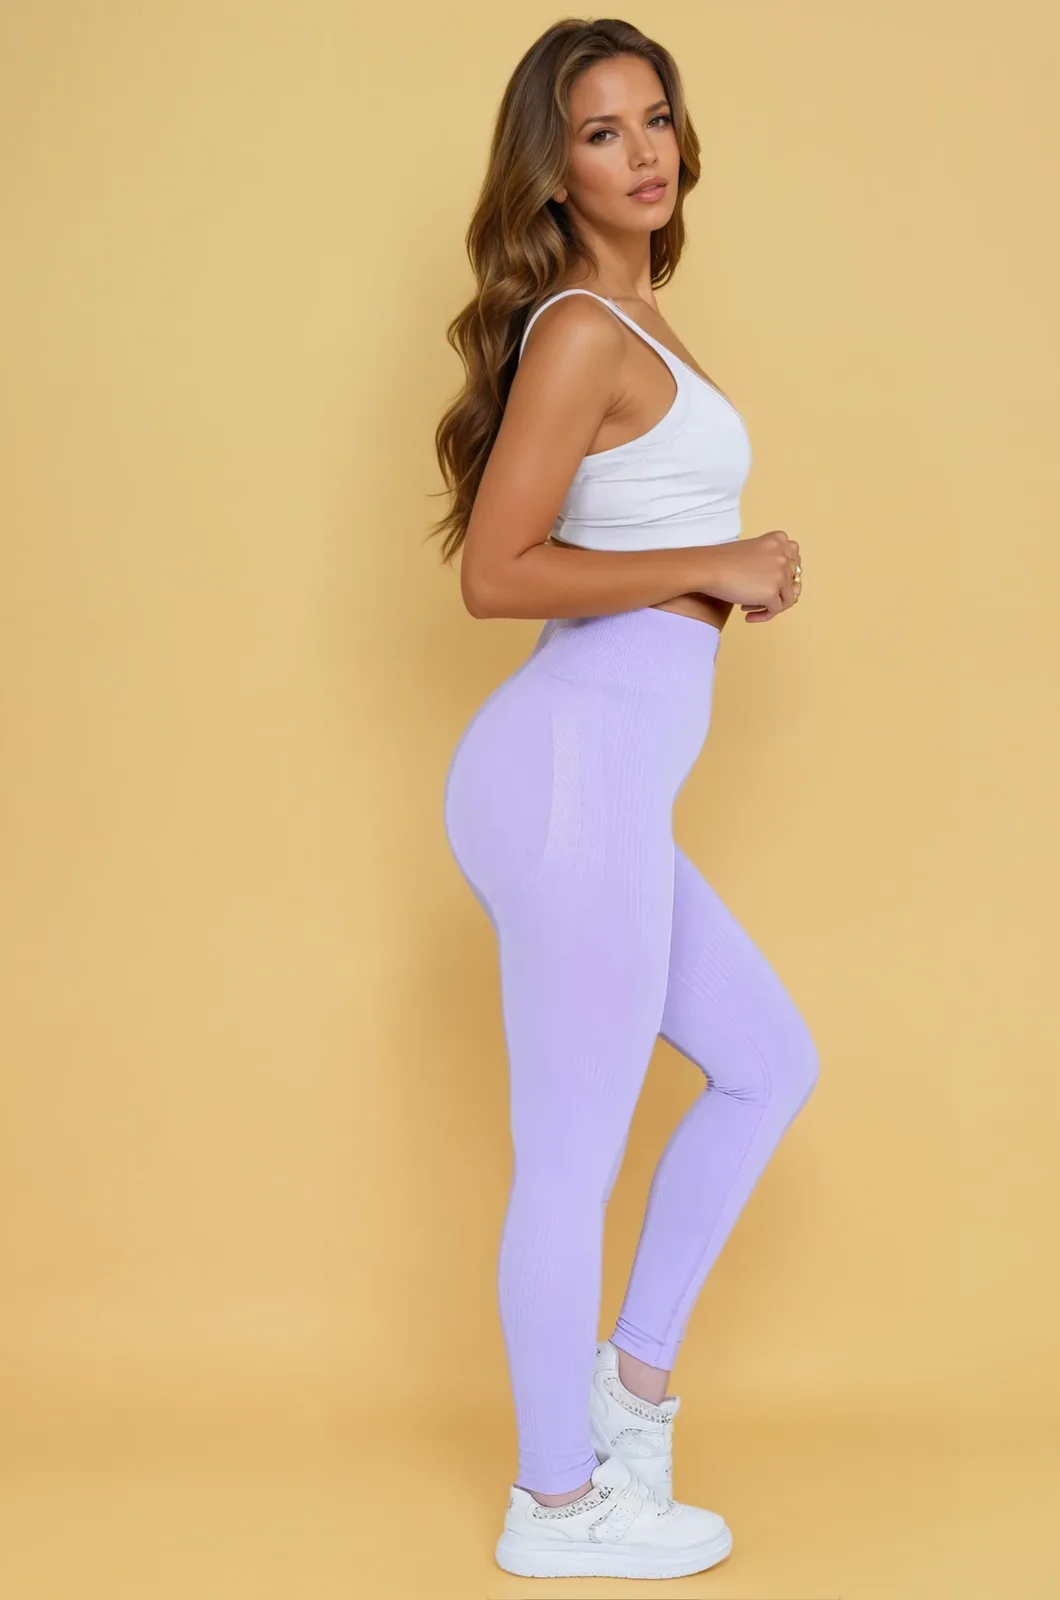
Custom seamless workout sets rely on body-mapped variable tension rather than restrictive seams. Here are the core private label architectures engineered regularly in our Istanbul circular knitting facility.
Constructed with zoned micro-ribbing down the lateral thighs and lateral torso. Uses high-modulus air-jet covered Lycra with air-textured Polyamide 6.6 to sculpt without pinching or rolling at the waistband.
Get Tech Pack & Spec SheetEngineered with open-knit pinhole jacquard beneath the bustline, along spinal sweat pathways, and behind knees. Maximizes kinetic air permeability during HIIT without sacrificing squat opacity.
Get Tech Pack & Spec Sheet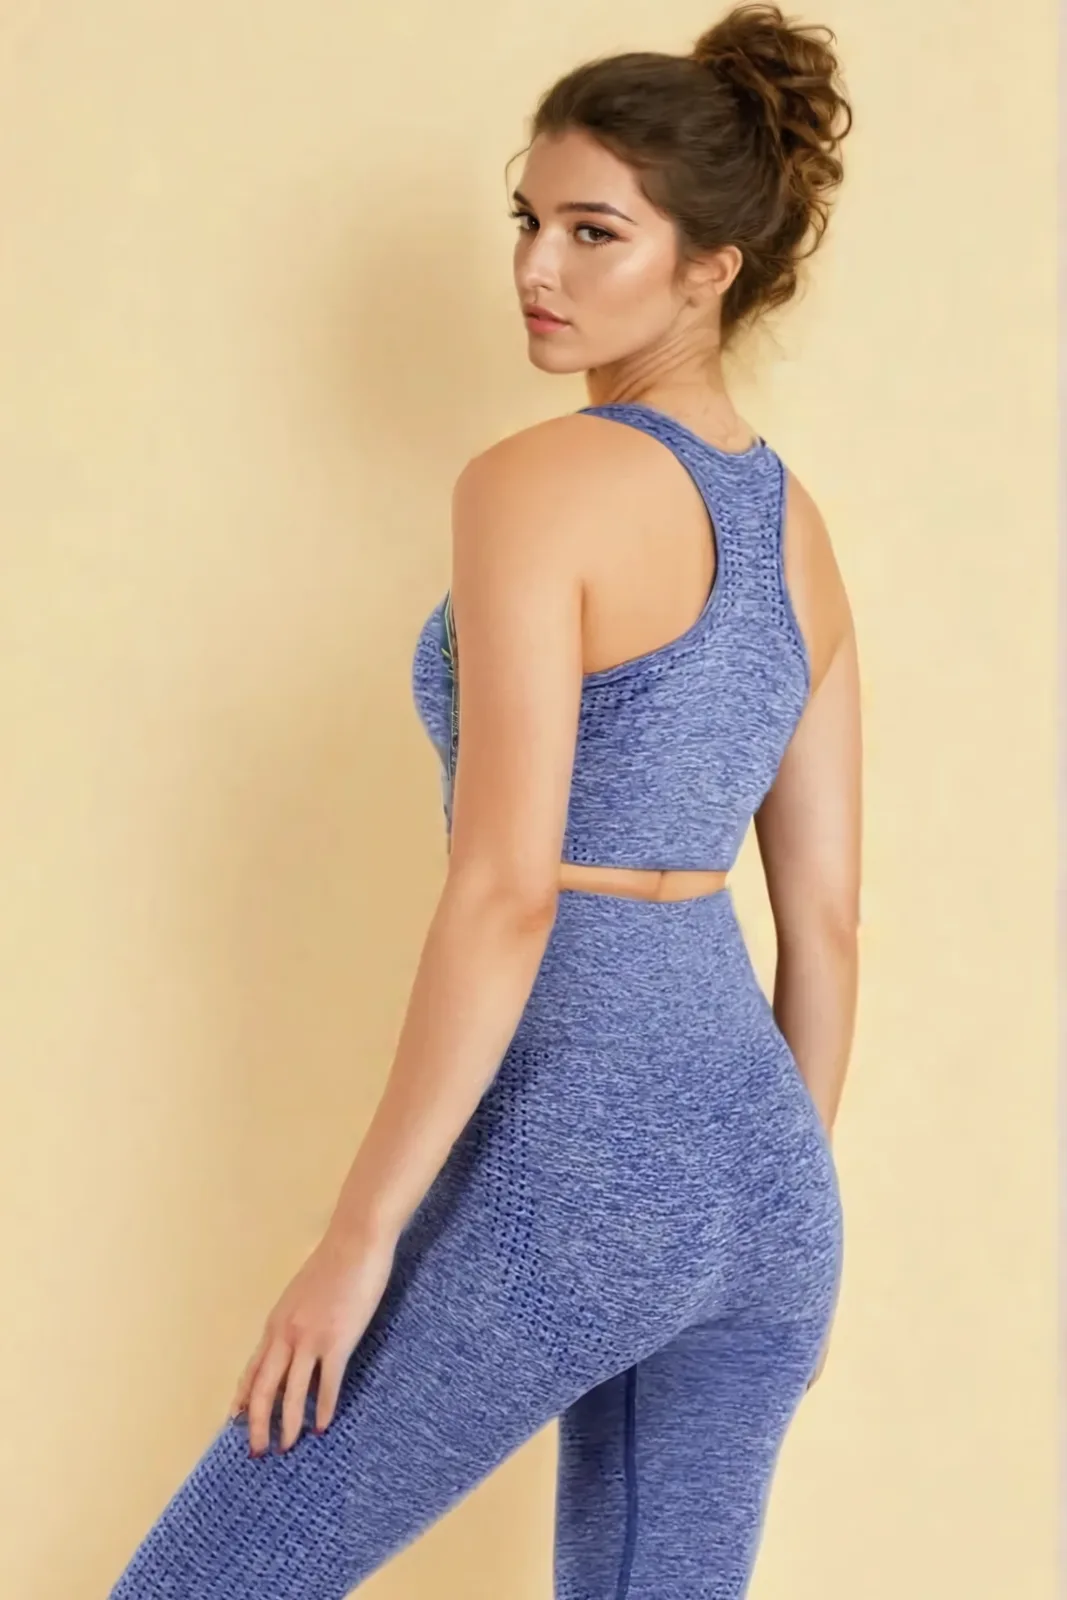
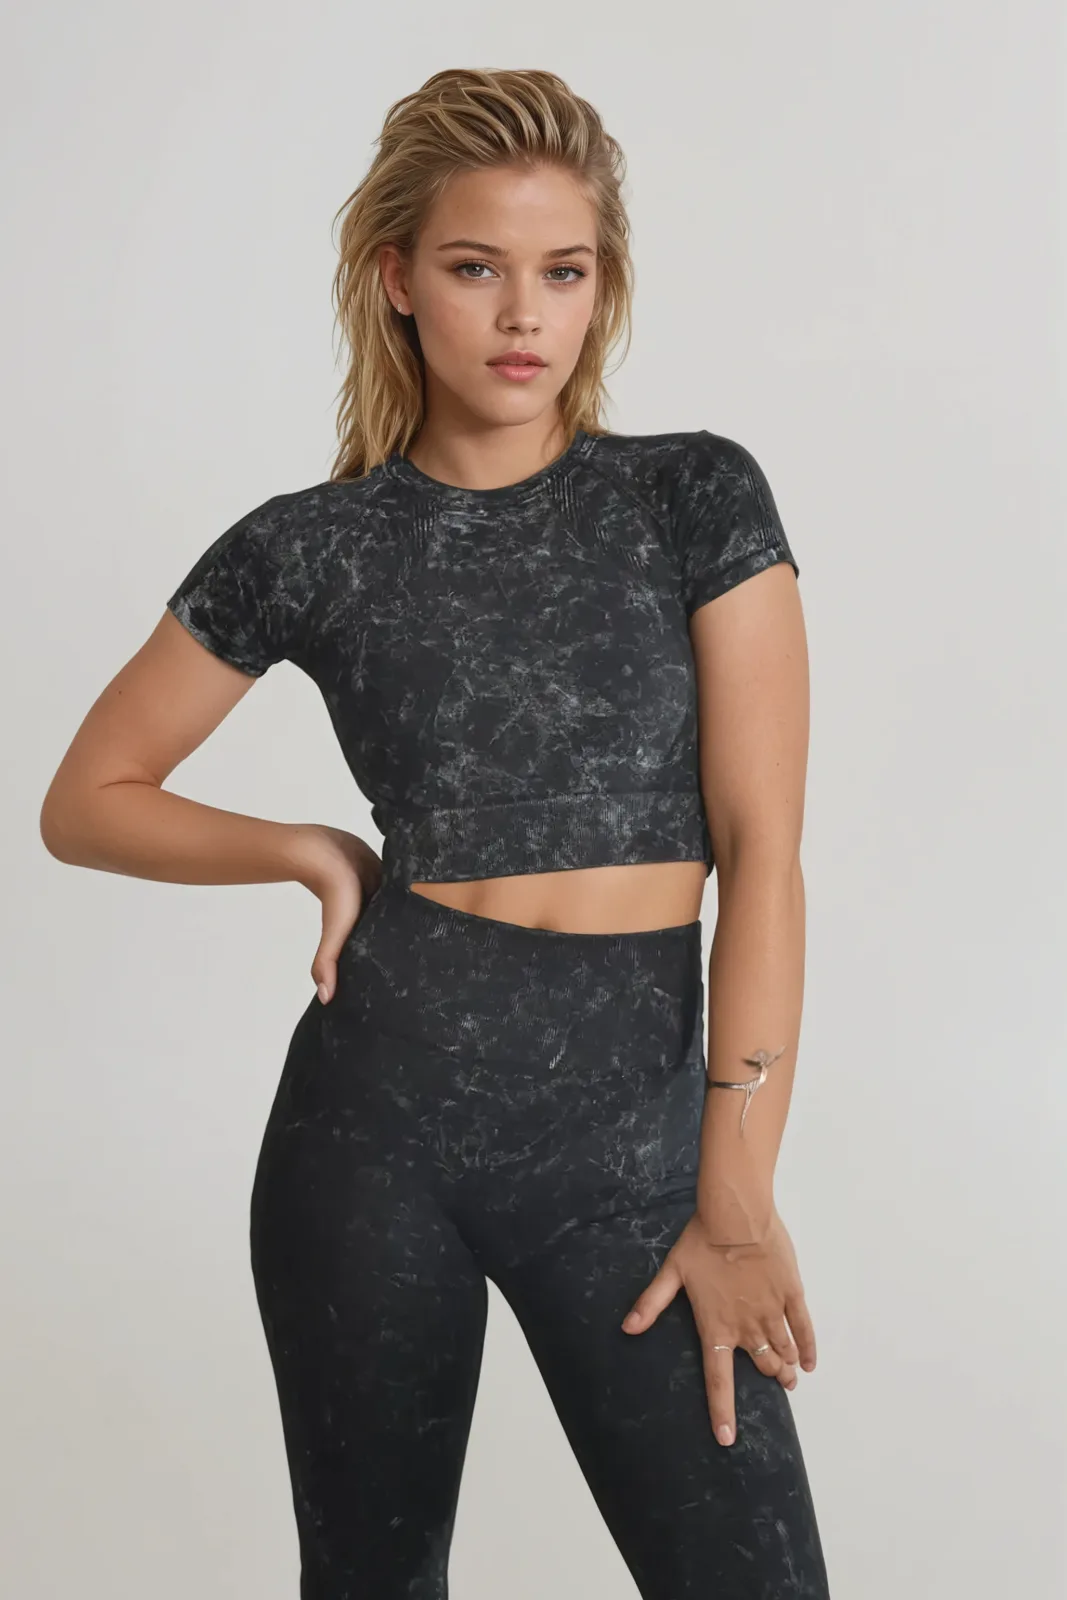
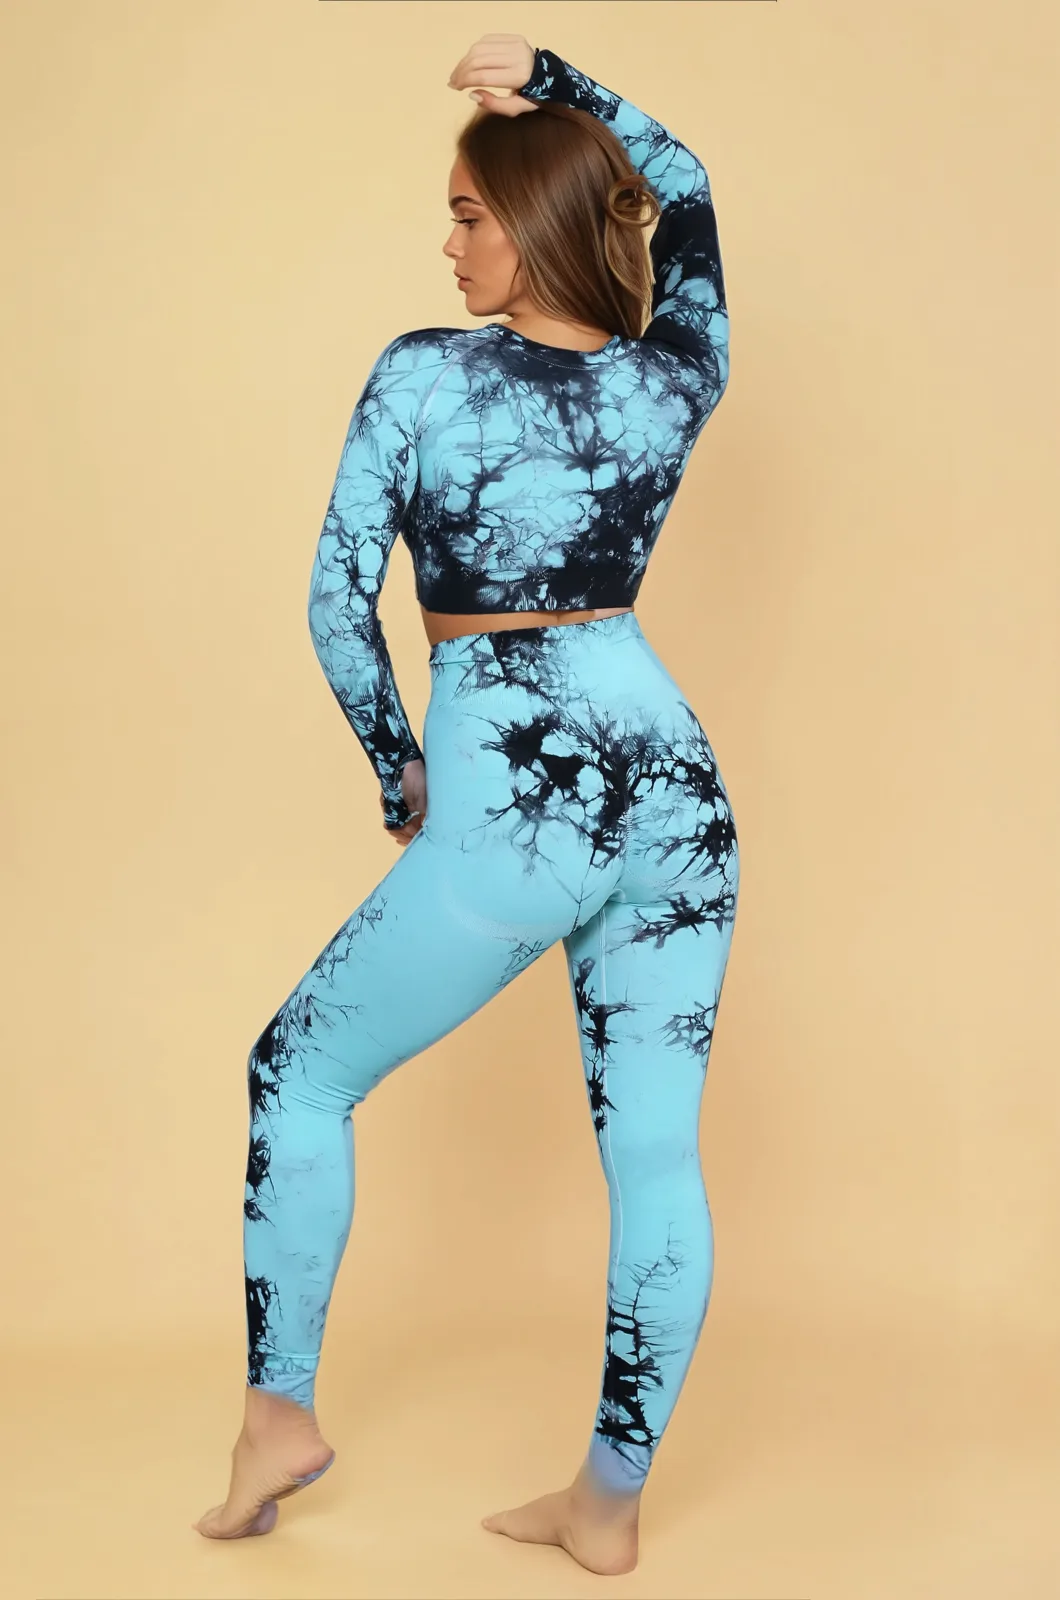
Knitted from dope-dyed marl yarns and cationic polyesters that yield organic heathered marl finishes directly off the machine cylinder, reducing wet processing environmental impact and water runoff.
Get Tech Pack & Spec SheetLooking for custom combinations such as cross-back sports bras paired with biker shorts, square-neck crop tops, or engineered shrugs? We configure seamless tubular diameters to your exact grading targets.
Get CatalogFuture Procurement Trends
Modern procurement directors are pivoting away from multi-tiered supply chains toward vertical circular knitters. Discover the strategic shifts shaping global activewear procurement.
Global supply disruptions and ocean transit volatility have caused European and East Coast US buyers to hedge long-haul Asian routes by shifting volume to Turkey, where direct highway networks supply Central Europe in under a week.
Impending EU Ecodesign (ESPR) mandates require apparel recycling feasibility. The industry is moving away from bonded multi-layer elastane towards mono-polyamide formulations that allow mechanical breakdown and re-spinning into circular yarn.
Activewear buyers now reject flimsy 20-gauge products prone to sheer deformation during squats. The new international commercial standard demands 28-gauge fine-loop knitting that maintains total opacity even under 140% multi-directional stretch.
Disparate fabric origins ruin matching workout sets. Modern procurement protocols require seamless bras and leggings to be knit from matched master yarn lots and dyed concurrently in identical dye-vats to eliminate shade dissonance under retail illumination.
Technological Evolution
Unlike traditional cut-and-sew garment making that wastes up to 20% of flat fabric offcuts, circular knitting shapes cylindrical tubes directly around bodily anatomy.
Santoni electronic sinkers dynamically alter needle density mid-cycle. This allows firm 450-denier abdominal support to blend imperceptibly into softer 120-denier glute release zones without introducing a single abrasive internal seam.
Tubular circular knitting knits precise garment contours, generating near-zero pattern waste compared to legacy cut-and-sew activewear markers. This lowers raw fiber spend and drastically curtails industrial textile landfill volume.
Without side overlock seams vulnerable to thread breakage under rigorous athletic strain, seamless activewear boasts exceptional longevity and burst strength, significantly cutting return rates for direct-to-consumer e-commerce brands.
Changing compression mapping, ventilation micro-structures, or surface jacquards involves adjusting machine programming files rather than retooling physical cutting tables, reducing counter-sampling cycles from weeks down to single days.
Comparative Matrix
Evaluate the exact manufacturing trade-offs between seamless circular knitting and traditional cut-and-sew processes to determine the right production vehicle for your collection.
| Evaluation Vector | Santoni Circular Seamless (Overfit) | Conventional Cut-and-Sew Assembly |
|---|---|---|
| Fabric Scrap Loss | Near zero; garment tubes are knitted to precise finished proportions | 15%–22% cutting offcut loss across nested patterns |
| Internal Chafe Risk | Zero lateral seams; flatlock thread only applied to inner leg and crotch gusset | Multiple structural seams (lateral, waist, armholes) cause friction points |
| Zoned Elasticity | Graduated compression programmed needle-by-needle into a single fabric face | Requires cutting and joining separate fabrics or bonding silicone tapes |
| Batch Color Cohesion | Bras and bottoms knitted from uniform batch yarn and dyed simultaneously | Tops and bottoms frequently cut from different dye lots, causing mismatch |
| Physical Sampling Time | 5 to 7 days direct via our 20 in-house Santoni machines | 15 to 25 days depending on roll fabric delivery and pattern drafting |
| Best Suited Categories | Form-fitting athletic sets, compression tights, molded sports bras, yoga apparel | Loose silhouettes, woven parkas, oversized fleece, multi-panel jackets |
Direct Factory Workflow
Every step of our production workflow operates under rigorous quality checks in Istanbul, ensuring consistent stretch, absolute color uniformity, and uncompromised structural integrity.
We source premium micro-polyamide 6.6, air-textured filaments, or recycled Q-NOVA® fibers, pairing them with covered spandex to establish target compression, hand-feel, and opacity.
Our knitting engineers digitize your sizing specifications and compression maps into machine-executable needle code. Physical samples are knitted, finished, and ready for your review within 5 to 7 days.
Your order is loaded onto our 20 Santoni Top2V cylinders. The body-mapped tubes are continuously knitted to length with integrated under-bust support bands, contouring ribs, and airflow perforations.
Seamless tubes undergo controlled overflow dyeing with certified partner mills, pass through precision gusset stitching, and receive heat-applied branding before being packaged into retail-ready presentation cartons.
Production Portfolio
The Overfit Edge
We are actual machine operators and textile engineers, not commission-based brokers. When you build your custom seamless workout sets with our team, you lock in measurable manufacturing advantages.
We own and run 20 Santoni Top2V circular knitting machines in Beylikdüzü, İstanbul. You speak straight to the technical crew programming the needles, eliminating third-party markups and miscommunications.
Because yarn preparation, sizing software, and circular machines operate under one direct factory roof, counter-samples are completed in 5 to 7 days, shaving months off typical retail launch timelines.
Our production minimum is 1,000 units per style, with the flexibility to split into 2 size curves and up to 3 lab-dip colors (e.g., 500 Medium and 500 Large across 2 distinct seasonal shades).
Located in Turkey's premier textile manufacturing hub, we deliver to major EU markets in days via ground freight under customs union privileges, bypassing lengthy multi-week ocean carrier delays.
Procurement FAQ
Get precise technical clarity on yarn densities, squat-proof testing, sizing tolerances, and global shipping protocols for custom seamless workout sets.
Our factory production MOQ is 1,000 pieces per style. Within this 1,000-piece production tier, you can configure up to 2 size gradings (e.g., S/M and L/XL) and split across up to 3 custom lab-dip colourways, giving direct-to-consumer and boutique brands supreme supply chain agility without ballooning holding costs.
Opacity in seamless knitwear is a mechanical engineering calculation. On our 28-gauge Santoni Top2V cylinders, we pair premium micro-polyamide 6.6 with double-covered elastane (spandex) under high interloop tension. This dense, multi-filament loop matrix prevents light refraction even under 140% biaxial stretch test parameters.
We eliminate color dissonance by knitting both pieces using the exact same master yarn batch and feeding both components into single-bath computerized overflow dyeing machinery. Tension variables are synchronized across cylinder programs to ensure both top and bottom age and perform identically.
Because programming, yarn stock, and 20 Santoni machines operate under one direct roof in Beylikdüzü, İstanbul, we do not depend on external subcontractors. Once your CAD or physical benchmark is received, master knit programming and physical counter-sampling take just 5 to 7 business days.
Yes, our capabilities include knitted-in Jacquard micro-logos, high-elongation silicone heat transfers, heat-seal interior neck labels, custom jacquard underbust bands, and OEKO-TEX certified compostable zip-lock retail polybags complete with your scannable UPC barcodes.
Istanbul bridges Eastern manufacturing precision with Western logistics agility. European activewear shipments transit by direct highway freight in 3 to 6 days under preferential customs union agreements, while air-cargo dispatches reach New York, Los Angeles, and London within 48 to 72 hours.
Launch Your Collection
Connect directly with our engineering division in Beylikdüzü, Istanbul. Share your benchmark sample or tech pack to receive raw material swatches, cost projections, and your initial sample set within 5 to 7 days.
Direct Factory Production · MOQ 1,000 Pcs Per Style · Sampling in 5–7 Days