Precision-engineered apparel produced on proprietary Santoni Top2V circular knits. Scalable wholesale runs with full brand integration, compressive mapping, and export-ready compliance.
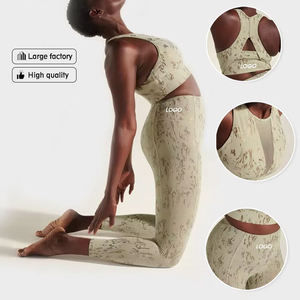
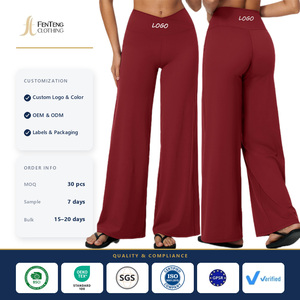
Why leading activewear labels are transitioning procurement from traditional flat-lock cut-and-sew to unified 28-gauge tubular seamless architecture.
In traditional activewear manufacturing, multi-panel garment architecture relies heavily on flat-lock stitching or bonded overlays to construct the legs, gusset, and waistband. These mechanical seams represent primary failure points during high-velocity elastic expansion (squat strain, lateral stretching) and generate significant friction against epidermis tissue during sustained athletic perspiration.
As an established private-label leggings manufacturer operating 20 specialized Italian Santoni Top2V circular machines in Beylikdüzü, İstanbul, Overfit Seamless utilizes continuous tubular feed processing. By adjusting yarn feed tensions and needle actions dynamically via integrated computer software, our production floor programs structural body-mapping, multi-tier graduated compression zones (e.g., higher mechanical resistance on the outer thigh and core support, combined with high-ventilation micro-mesh textures across popliteal areas) directly into a continuous knit tube. The result is zero longitudinal lateral seams, non-restrictive 4-way elastic stretch, and total elimination of seam-chafing.
Furthermore, seamless engineering minimizes virgin material cutting scrap from the historical 18–24% observed in conventional garment markers down to less than 2.8%, dramatically curbing overhead yarn cost while meeting stringent corporate Environmental, Social, and Governance (ESG) standards across the EU and North American retail distribution networks.
| Performance Vector | Proprietary Seamless Circular (Santoni 28G) | Conventional Cut-and-Sew |
|---|---|---|
| Structural Integrity | Single-tube continuous yarn matrix; no lateral seam splitting | Multiple sewn panels; high risk of thread snapping under 150%+ strain |
| Targeted Ergonomic Fit | Direct stitch programming for lumbar, abdominal, & glute shaping | Requires piecing cut darts, external elastic bands, and bulky seams |
| Material Efficiency | <3% waste; high yield through computerized shaped tubular knit | 18% - 24% fabric waste left on spreading and cutting tables |
| Prototyping Agility | 5–7 days turnaround; digital stitch modification on floor machines | 14–25 days; manual paper pattern cutting, sizing, and multi-run sewing |
| Hydrodynamic Comfort | Smooth interior skin-contact zone; no abrasion or chafe lines | Seam ridges accumulate sweat and abrasive rubbing during workouts |
Strategic analysis for category procurement managers, sourcing executives, and private label founders preparing their catalogs for next-generation consumer demand.
Procurement volume is rapidly shifting from crude oil-derived polymers toward certified pre- and post-consumer regenerated Nylon 6.6 (ECONYL® equivalents) and bio-based Polyamide variants. Brands demanding durable 300+ wash cycles without fiber fatigue are selecting high-filament micro-polyamide blended with targeted ROICA™ or Creora® elastane to guarantee non-sheer, squat-proof opacity down to 220 GSM.
The divide between functional gym performance gear and premium lifestyle apparel has collapsed. High-rise crossover waistbands, gentle flared hems, and wide-leg active trousers must now balance compressive pelvic alignment with high-drape softness. Sourcing departments seek suppliers capable of executing melange aesthetic texturing alongside clinical recovery tensions.
With high interest rates and retail stock obsolescence eating away at enterprise margins, 120-day ocean freight lead times from East Asia have become untenable. Sourcing out of İstanbul, Türkiye offers zero-tariff entry into the European Customs Union via road transit within 4–7 days, drastically reducing inventory safety buffers while elevating stock replenishment cycles.
Direct manufacturer control from initial yarn spinning and pantone lab-dips to tubular circular execution, branding, and export logistics.
We operate 20 dedicated Santoni Top2V circular knitting machines in Beylikdüzü, İstanbul. We do not broker manufacturing or rely on third-party subcontractors; all knitting occurs under direct engineering supervision.
Direct access to on-site machine programmers allows us to translate digital tech packs or physical benchmark samples into fully functional counter-samples within 5 to 7 operational days.
Standard enterprise production starts at an accessible 1,000 pieces per style. Brands can freely split their volume across up to 2 distinct sizing tiers and 3 bespoke lab-dipped color profiles.
İstanbul's strategic hub allows door-to-door delivery across continental Europe in days via direct truck lines, coupled with fast Atlantic sea-freight lanes to the United States and North American distribution ports.
Key operational facts regarding MOQ frameworks, yarn chemistry, private-label branding, and international trade documentation.
We are an original equipment manufacturer (OEM/ODM). We run 20 Italian Santoni Top2V circular knitting machines at our primary plant in Beylikdüzü, İstanbul. We do not resell stock items; every order is knitted from raw yarn according to your brand's technical specifications and private labeling.
Our baseline MOQ is 1,000 units per style. To support catalog depth, we permit you to subdivide that 1,000-piece commitment into up to 2 size tiers (e.g., 500 Medium / 500 Large) and across up to 3 customized colorways, streamlining balance between inventory capital and consumer choice.
Because machine programming and knitting execution are kept entirely in-house without third-party delay, prototype samples are typically completed within 5 to 7 business days following tech pack lock-in and yarn selection.
We offer total turnkey brand customization: integrated jacquard knit logos, silicone thermal transfer prints, high-stretch heat seal neck labels, custom woven waist tags, bespoke pantone dyeing, eco-poly packaging bags, and pre-applied barcode hangtags ready for 3PL warehouse fulfillment.
We calibrate gauge, loop density, and core-spun elastane yarn content (typically between 12% and 22% high-denier elastane wrapped in polyamide 6.6). Every batch undergo multi-directional stretch-opacity testing on floor stretch mannequins to guarantee zero grin-through or transparency under direct athletic lighting.
Under the EU-Türkiye Customs Union framework, industrial goods manufactured in Türkiye enjoy preferential duty-free movement into the European Union with ATR documentation. Furthermore, deliveries to major European hubs take only days via overland freight, while fast sea routes serve East Coast US ports significantly faster than traditional trans-Pacific container shipping.
Send us your target tech pack, reference garment specifications, or color concept. Our engineering team in İstanbul will review your yarn properties, output realistic timeline matrices, and mail counter-samples directly to your headquarters.