Explore our export-grade seamless inventory frameworks. Every piece is precision-programmed on circular Santoni machines to integrate localized muscle compression, dynamic rib support, and hyper-breathable venting zones directly into the seamless knit structure.
Operating out of Beylikdüzü, İstanbul since 2019, our factory integrates Italian Santoni circular knitting machinery, localized dyeing labs, and streamlined European logistics to eliminate intermediaries and secure factory-direct margins.
We do not outsource knitting. Our high-precision 28-gauge circular Santoni machines program gradient compression, micro-mesh breathability, and contour ribbing directly into a seamless tubular structure, eliminating chafe-inducing side seams and maximizing garment integrity.
Transition from concept sketches or physical benchmark garments to finished, wearable prototypes within 5 to 7 business days. Our proprietary Santoni SM8 software programming runs parallel with our internal yarn inventory for lightning-fast lab dip and sample validation.
Strategically situated in Turkey, our production facility offers rapid European road-freight transit in just 3 to 6 business days, sidestepping the unpredictable 45-day ocean freight delays associated with Far-East sourcing, and enjoying EU Customs Union duty-free benefits.
Factory Verification Guarantee: Every batch of bulk seamless leggings undergoes rigorous mechanical and chemical inspection protocols. Our testing covers burst strength (ASTM D3787), elongation recovery (ASTM D2594), colorfastness to perspiration (ISO 105-E04), and squat-proof opacity spectrophotometry (CIE LAB).
An in-depth technical analysis for apparel sourcing directors, supply chain VPs, and technical design teams evaluating the shift from cut-and-sew apparel to seamless circular engineering.
Traditional cut-and-sew activewear manufacturing suffers from structural vulnerabilities: lateral seams impose friction against the epidermis during intense kinetic movement, seam overlocks cause elastane fatigue, and marker waste typically discards between 14% and 22% of virgin textile yardage. Seamless circular knitting radically transforms this production paradigm. Utilizing state-of-the-art electronically controlled circular knitting machines—specifically the industry gold-standard Santoni Top2V 28-gauge—garments are constructed as continuous, three-dimensional tubes where variations in tension, yarn feeding, and stitch architecture are controlled at the individual needle level.
In our İstanbul knitting facilities, seamless leggings are engineered using Air-Covered Yarns (ACY), combining micro-denier Nylon 6.6 with premium Spandex filaments (70D/24F Polyamide wrapped around 40D or 70D Elastane). This dual-filament configuration achieves optimal hysteresis recovery, delivering an instantaneous modulus rebound that eliminates knee sagging, waistband roll-down, and stress bagging after repetitive gym sessions. By dynamically altering the knit structure across the needle cylinder, our engineers embed distinct functional performance zones into a single monolithic garment:
Engineered higher-tension interlock loops at the ankle gradually soften into micro-rib structures at the calf and thigh. This graduated pressure gradient supports venous blood return, suppresses muscle oscillation during plyometrics, and mitigates post-training fatigue without restricting arterial flow.
Integrated bird-eye and open-mesh jacquard zones are mapped directly across the popliteal fossa (behind the knee) and lower lumbar zones. These micropores maximize forced convective cooling, expediting latent heat loss and sweat evaporation at rates up to 48% higher than planar jersey.
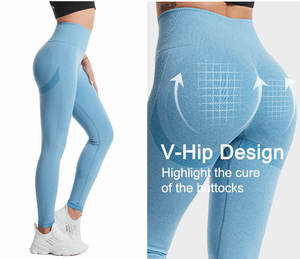
Utilizing high-density float stitches and parabolic tuck-stitch contours underneath the gluteal fold, our machine programs create localized tension contrast. This delivers structural glute-lifting aesthetics without requiring bulky external seams or uncomfortable silicone banding.
| Performance Characteristic | High-Gauge Seamless Circular Knit | Standard Cut-and-Sew Flatlock | Testing Standard / Metric | B2B Sourcing Advantage |
|---|---|---|---|---|
| Bursting Strength | > 420 kPa | 280 – 320 kPa (Seam Vulnerability) | ASTM D3787 (Ball Burst Test) | +38% Durability Eliminates blowouts during high-intensity squats |
| Cut & Fabric Yardage Waste | 1.8% – 3.2% (Tubular Form) | 16.5% – 22.0% (Marker Scraps) | Mass Balance Efficiency Audit | ESG Optimized Direct reduction in raw fiber procurement costs |
| Epidermal Friction Index | 0.12 µ (Smooth Internal Surface) | 0.38 µ (Raised Overlock Junctions) | Rotational Skin Abrasion Model | Zero-Chafe Superior rating in marathon & hot yoga user trials |
| Modulus Hysteresis Loss | < 4.2% After 2,000 Cycles | 9.5% – 14.0% After 2,000 Cycles | ASTM D2594 (Elastic Stretch Recovery) | Shape Retention Retains firm silhouette across multi-season consumer wear |
| Moisture Vapor Transmission (MVTR) | > 9,800 g/m²/24h | 6,200 – 7,100 g/m²/24h | JIS L 1099 B-1 (Inverted Cup) | Rapid Dry Eliminates sticky sweat traps via localized micro-mesh |
Strategic purchasing insights to help brand directors maintain margin resilience, stay ahead of tightening EU eco-regulations, and capture market share in a fast-evolving athleisure landscape.
Global regulatory bodies, spearheaded by the EU Corporate Sustainability Due Diligence Directive (CSDDD), are placing fossil-based virgin synthetics under heavy scrutiny. Forward-looking brands are transitioning to post-consumer regenerated polyamides, such as Q-NOVA® and ECONYL®, paired with degradable bio-elastanes. Bulk seamless leggings manufactured with pre-dyed dope yarn drastically diminish freshwater consumption and chemical runoff, ensuring seamless alignment with upcoming Digital Product Passport (DPP) standards.
The era of booking rigid 6-month Asian ocean-freight cycles is coming to an end. Escalating geopolitical bottlenecks in primary maritime choke points have triggered severe inventory stockouts for activewear brands. Sourcing from European production hubs like Turkey gives brands an agile 'Just-In-Time' replenishment capability. Short production runs of 1,000 units per style allow apparel merchants to test fresh seasonal colorways with minimal capital exposure, restocking hot sellers in a matter of days.
Consumers increasingly expect high-performance workout leggings to pull double duty as refined casual wear. This evolution has prompted surging wholesale demand for ribbed lounge sets, flare trousers with integrated high-rise compression, and subtle melange mineral washes. Leggings featuring built-in pockets knitted directly into the hip without bulky sewing represent one of the fastest-growing OEM design requests from mid-to-high luxury fitness brands.
Predictive Purchasing Takeaway: Seamless activewear that relies on superficial chemical top-coats for wicking washes out within 15–20 laundry cycles. By contrast, activewear engineered with modified cross-section fiber architecture (e.g., grooved trilobal filaments) provides permanent capillary moisture management that endures throughout the lifetime of the garment—substantially curbing consumer return rates on e-commerce platforms.
From initial design blueprint to warehouse delivery, our tightly controlled in-house vertical process delivers complete quality certainty at every stage of production.
We source premium micro-denier polyamides and covered Lycra to match your exact handfeel and compression requirements. Custom lab dip dyeing delivers precise Pantone PMS matching within 72 hours.
Our CAD engineers translate tech packs or reference samples into Santoni SM8 machine code. In-house knitting allows us to complete initial counter-samples in 5–7 days for client fit review.
Leggings are tubular-knitted across 20 Santoni Top2V circular machines. Each cylinder is monitored for needle deflection and yarn tension to guarantee zero line-breaks and pristine surface consistency.
Garments undergo automated boarding, flatlock gusset attachment, heat-transfer private labeling, spectrophotometer shade verification, and barcoded polybagging before rapid dispatch from İstanbul.
Direct, transparent answers covering minimum order commitments, technical tolerances, testing methodologies, and custom private-label branding execution.
Our standard manufacturing baseline is 1,000 pieces per style. Crucially for growing brands, this minimum can be divided across up to 2 distinct sizes and up to 3 individual colorways (for example: 500 units in Size S/M and 500 units in Size L/XL, split across Forest Green, Pitch Black, and Burnt Terracotta). This balanced threshold lets brands launch comprehensive collections while keeping our circular Santoni knitting banks at peak operational efficiency.
Opacity failures typically occur when low-gauge knitting (e.g., 20G or 24G) is paired with under-twisted, single-ply yarns. We eradicate sheer stretch by running high-density 28-gauge Santoni cylinders alongside dual-ply Air-Covered Poly/Elastane yarns, maintaining a finished fabric mass between 300 and 340 GSM. Every batch undergoes a standardized biaxial mechanical stretch test against high-lux optical sensors to ensure total opacity at peak extension.
Because all 20 Santoni Top2V machines, CAD programming suites, and yarn inventories are managed under one roof in our Beylikdüzü factory, prototype samples are ready in just 5 to 7 business days. We do not depend on third-party contractors for sampling, enabling rapid revisions to waistband height, crotch gusset fit, or rib compression zones without derailing your launch calendar.
We provide full-spectrum OEM and private-label customization: silicone heat-transfer logos, custom jacquard designs knitted directly into waistbands, reflective safety accents, branded wash-care labels, eco-friendly FSC-certified hangtags, and custom recycled frosted polybags. We can also integrate anti-slip interior silicone waist grips to ensure zero rollover during sprint drills.
Turkey combines decades of European textile craftsmanship with significant logistical efficiencies. Shipments to EU logistics hubs arrive within 3 to 6 days via express road transit, cutting out the typical 45-day maritime container backlog. Furthermore, under the EU–Turkey Customs Union, textile shipments enter the EU without industrial customs tariffs, reducing landing costs and dramatically streamlining seasonal cash flow.
We operate an AQL 1.5/2.5 inspection protocol. Every individual production run is audited for: 1) dimensional stability following repeated laundering (AATCC 135), 2) bursting resistance (ASTM D3787), 3) color fastness to wash and perspiration (ISO 105-C06/E04), and 4) stitch elasticity along the crotch gusset junction to prevent blowout vulnerabilities under dynamic stress.