Precision Seamless Circular Engineering, Global Export Compliance, and Scalable OEM/ODM Solutions for High-Performance Athleisure Brands
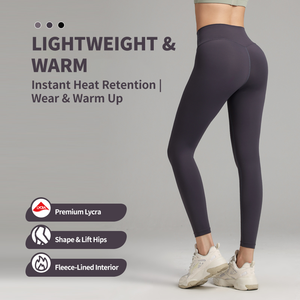
Ergonomically engineered using advanced tubular circular knitting. Our flagship high-waist series combines targeted anatomical compression, high-elasticity recovery, and micro-ribbed posture support.
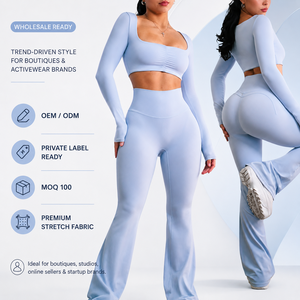
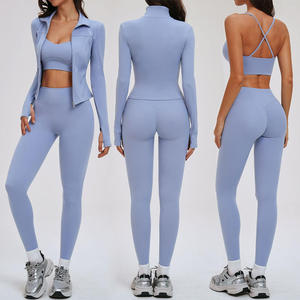
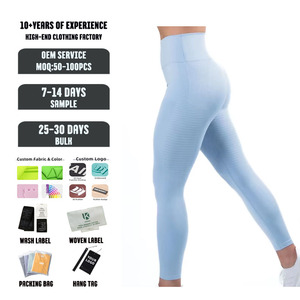
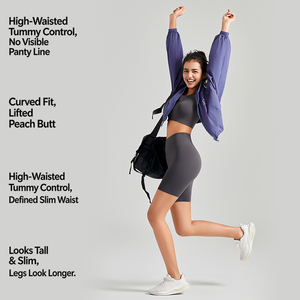
In high-performance sportswear manufacturing, the engineering of the high-waist band is the benchmark for structural quality. Traditional cut-and-sew assembly relies on elastic inserts fixed with rigid flatlock or coverstitch seams, inevitably causing localized pressure, friction hot-spots, and elastic degradation over repetitive laundry cycles. Our seamless circular knitting protocol completely reconfigures this dynamic.
Using multi-feed, computer-controlled Santoni circular knitting machines (Gauge 28), we map functional zones directly into the knit matrix. The waistband transitions dynamically from a high-modulus compression core to a low-tension ergonomic edge without a single connecting seam. This produces true graduated compression: gentle abdominal support that prevents rollover during squats and dynamic lateral movements, coupled with uninhibited diaphragmatic breathing.
| Engineering Attribute | Seamless Circular Knit (Our Standard) | Standard Cut-and-Sew |
|---|---|---|
| Fabric Continuity | Zero side-seam tubular construction; integrated compression pockets | Requires 4-way panel cutting, leading to seam chafing |
| Waistband Mechanics | High-density covered elastane woven into double-layer ribbed jacquard | Overlocked elastic band prone to twisting and roll-down |
| Material Efficiency | Under 2.5% yarn cut-off scrap rate (Eco-conscious) | 18% - 24% fabric waste through traditional pattern nesting |
| Tensile Strength Retention | >95% recovery after 5,000 dynamic cycle tests (ASTM D4964) | Prone to thread cracking along lateral structural seams |
Direct-to-factory engineering eliminates trading broker margins, streamlines technical tech-pack interpretation, and delivers reliable cycle times for medium-to-large consumer activewear labels worldwide.
Our workshop houses dedicated high-speed circular machinery running round the clock. Retaining absolute control over needle calibration, air-jet tension, and stitch architecture guarantees zero lot-to-lot variance across 100,000+ unit runs.
Direct programmer-to-machine communication enables ultra-fast tech-pack sampling. We translate 3D CAD patterns or physical sample benchmarks into compiled machine punch files within 48 hours, delivering counter-samples in 5 to 7 business days.
From dope-dyed virgin Polyamide 6.6 to post-consumer recycled nylon and Spandex, all filament inputs carry OEKO-TEX Standard 100 and Global Recycled Standard certifications, meeting the compliance requirements of North American and EU retail.
Every fabric roll and seamless tube lot undergoes strict 2-axis stretch opacity inspection under 1,000-lux halogen lamps. We guarantee zero grin-through and squat-proof reliability even at 160% maximum tensile stretch.
We combine production scale with flexible brand support. Standard runs start at 1,000 units per style (split across sizes/colorways), supported by direct freight links out of Ningbo and Shanghai ports, alongside DDP air express solutions.
The athleisure market is moving past generic polyester/spandex blends. Brand buyers must align their supply lines with the next phase of high-waist activewear engineering.
International environmental regulations (including EU Digital Product Passports) are accelerating demand for closed-loop Nylon 6 filaments. Forward-thinking procurement strategies balance mechanical stability with post-consumer recycled waste content to lower carbon footprint metrics.
Consumer preferences have evolved from basic planar leggings to complex 3D surface architecture. By combining localized drop-needle knitting, variable-density ribbing, and ruched butt-sculpt ruching, manufacturers can create garments that shape natural curves without stiff internal wiring.
Post-pandemic athleisure blends cross-training gym use with all-day casual wear. Strategic micro-mesh jacquard perforations, knitted across high-perspiration zones such as the lower back and behind the knees, deliver targeted cooling and accelerated evaporation.
Essential answers to the core technical, compliance, and ordering questions encountered by sourcing managers and brand founders.
Roll-down happens when yarn tension is unbalanced or the waistband lacks graduated structural density. We counter this by pairing high-denier elastane core-spun yarns with a double-faced ribbed jacquard knit. This delivers firm mechanical recovery that holds its shape against movement without relying on restrictive top rubber bands.
Our standard production MOQ is 1,000 units per style, with the flexibility to split across up to 2 distinct sizes and up to 3 tailored pantone colors. Proto sampling and counter-fit development take 5 to 7 working days once tech-pack metrics and yarn specifications are confirmed.
Yes. Producing matching sports bras, crop tops, and leggings demands precise yarn dye-lot management. We knit matching tops and bottoms using identical raw yarn lots and dye batches, preventing the slight color casts and compression differences common across split factory lines.
We provide end-to-end OEM and ODM branding options. These include knitted-in jacquard brand motifs, high-stretch silicone heat transfers, laser-cut custom hangtags, branded bio-poly packaging, and certified recycled wash care labels sewn directly into gusset seams.