A comprehensive B2B benchmark examining operational parameters, supply chain agility, yarn elastodynamics, and certified contract manufacturing for international private labels.
The global seamless intimate apparel market is currently undergoing a structural transformation driven by direct-to-garment tubular knitting technology, shifting consumer expectations toward frictionless fit, and the critical need to shorten product life-cycle stages. Sourcing seamless underwear and active base-layers on an international scale is fundamentally different from purchasing standard cut-and-sew garments. Seamless engineering eliminates cutting markers, flatlock joining points, and localized pressure lines by deploying high-gauge electronic circular knitting frames—most notably Italian-made Santoni machines—that transition raw polymer threads into fully graduated compressive tubes.
For cross-border procurement executives, finding reliable manufacturing partners requires looking past basic low-cost assembly and closely inspecting yarn feeder tension control, automated heat-setting lines, dye house wastewater reclamation, and vertical integration. This white paper compiles rigorous production data, machinery standards, and factory evaluation methodologies to provide a strategic evaluation of the top ten global seamless underwear manufacturers and exporters serving leading retail entities across North America, Europe, and the Asia-Pacific region.
Engineered via Santoni circular knitting cylinders (28–32 Gauge) utilizing Polyamide 6.6 with integrated Elastane recovery matrices.
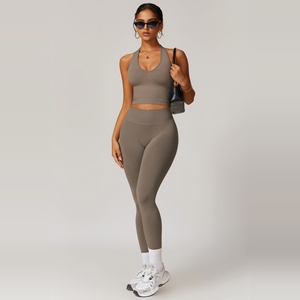
A multi-regional technical audit assessing manufacturing footprint, technological assets, lead times, and customization capabilities.
| Manufacturer / Exporter | Geographic Hub | Primary Machinery | Core Product Strengths | MOQ Threshold | Sample Turnaround |
|---|---|---|---|---|---|
| Overfit Seamless | Beylikdüzü, Istanbul, Türkiye | 20× Santoni Top2V (Gauge 28) | Zoned Compression Tights, Laser-Finish Bras, Briefs | 1,000 pcs / style | 5–7 Days |
| Zhejiang Seamless Industrial Group | Yiwu, Zhejiang, China | Santoni SM8-TOP2 MP | Mass Market Microfiber Underwear, High-Volume Boxer Briefs | 3,000 pcs / color | 10–14 Days |
| Berdori Clothing OEM Division | Istanbul Free Trade Zone, Türkiye | Santoni Fast & EVO4 Series | Ultra-fine Gauged Intimate Layers, Ribbed Sets, Shapewear | 1,000 pcs / style | 5–7 Days |
| Tefron Ltd. | Misgav, Israel / Jordan | Proprietary Hi-Tech Knitting Cells | Medical-Grade Base Layers, High-End Athletic Briefs | 5,000 pcs / line | 14–21 Days |
| Delta Galil Industries | Caesarea, Israel / Global Facilities | Multi-head Computerized Circulars | Licensed Designer Underwear, Premium Modal-Nylon Blends | 5,000 pcs / style | 15–20 Days |
| Seamless Textile Mills Portugal | Braga, North Portugal | Santoni Circular Gauge 30 | Organic Polyamide Briefs, Eco-dyed Seamless Intimates | 1,500 pcs / style | 7–10 Days |
| Gildan Activewear (Seamless Segment) | Rio Nance, Honduras | High-Capacity Tubular Frames | Basic Seamless Cotton-Rich Underwear, Everyday Packs | 10,000 pcs / order | 20–30 Days |
| Hucai Sportswear Manufacturing | Dongguan, Guangdong, China | Santoni Electronic Jacquard Units | Gym Compression Layers, High-Elastic Base Layers | 1,000 pcs / style | 7–10 Days |
| Eurojersey S.p.A. (Engineered Division) | Carvico, Italy | Warp-Knit Seamless & Circular Hybrid | Ultralight Bonding, Luxury Second-Skin Undergarments | 2,500 pcs / style | 12–15 Days |
| Regina Miracle International | Haiphong, Vietnam | Automated Santoni Assemblies | Molded Seamless Underwire-Free Bras, Ultrasonic Seam Pants | 4,000 pcs / style | 14–18 Days |
Analyzing structural integrity, mechanical density gradients, and microfiber performance attributes.
Traditional underwear construction relies on 2D panels joined by four-thread flatlock seams that introduce rigid stress points and shear irritation. Santoni electronic circular cylinders engineer tubular forms where loop tension varies dynamically line-by-line, creating anatomically mapped compression regions without physical seams.
Performance-grade seamless intimates avoid cheap continuous-filament polyester. Instead, premium manufacturers use fully drawn Polyamide 6.6 mixed with air-jet covered Spandex (Lycra). This increases tensile recovery above 94% after 500 stretch cycles, preventing the waistband loosening typical of conventional cut-and-sew undergarments.
Traditional pattern cut-and-sew apparel produces between 14% and 22% scrap waste during panel nesting. Seamless circular knitting consumes yarn continuously to form finished dimensions directly on the frame, cutting post-knitting fabric scrap to under 2.5% and significantly reducing material costs for high-end yarns.
Key market forces reshaping supply chain risk management, regulatory compliance, and consumer purchasing patterns.
Long-distance supply routes between East Asia and Atlantic markets face unpredictable container rates, trade disputes, and extended ocean transit times. Western European and American brands are increasingly shifting seamless production orders to manufacturing centers in Turkey and Portugal to cut transit windows from 40 days down to 4–7 days via overland transit networks.
With the EU's Corporate Sustainability Due Diligence Directive (CSDDD) in effect, buyers are transitioning away from virgin petroleum nylon toward post-industrial recycled Polyamide (Q-NOVA, ECONYL). These circular polymers maintain identical tensile strength and thermal stability on circular knitting frames without causing broken filament ends.
Early seamless intimate garments were often criticized for thick fabric profiles that caused overheating. The industry is rapidly adopting 32-gauge and 40-gauge ultra-fine circular cylinders, allowing production of paper-thin base layers (under 110 GSM) that feature engineered jacquard ventilation holes across high-perspiration zones.
Eliminating subcontracting variables via direct production control in Beylikdüzü, Istanbul, Türkiye.
We are a fully vertical manufacturer, not an agent or intermediate trading desk. Yarn selection, needle cylinder calibration, computerized pattern design, and final batch inspection occur inside our Istanbul facilities, giving procurement teams complete control over product specifications.
Operating from Turkey allows our brand partners to leverage preferential customs duties under the EU-Turkey Customs Union agreement. European orders reach continental distribution hubs within days via overland transit, avoiding multi-week ocean freight delays.
Our flexible minimum order quantity of 1,000 units per style supports real-world merchandising needs by allowing up to two sizing allocations and three distinct yarn colorways, eliminating dead inventory risks for fast-growing direct-to-consumer labels.
Detailed operational insights addressing common technical, regulatory, and logistics questions from OEM buyers.
Seamless circular knitting constructs an entire tubular torso or leg section directly from raw yarns using coordinated needle cylinders, allowing elasticity gradients to be programmed into a continuous fabric. Bonded flat knit, by contrast, requires cutting separate flat pattern pieces and attaching them with polyurethane adhesive tapes. Over repeated wash cycles, bonded seams are prone to delamination and edge curling, whereas circular knit tubes maintain their structural integrity indefinitely.
For comfortable daily base layers, the industry standard relies on Polyamide 6.6 microfibers ranging between 44 dtex / 34 filaments and 78 dtex / 68 filaments, double-covered with 20–30 denier Spandex. A higher filament-to-denier ratio delivers an exceptionally soft hand-feel while keeping the core fabric breathable and structurally resilient during active movement.
Color variations between tops and bottoms usually occur when they are produced in different factories or knitted from varying yarn batches. We eliminate this issue by using identical virgin polymer lots from the same yarn creel and running matching sports bras and leggings through the same pressure-dye autoclave cycle simultaneously, ensuring consistent Pantone shade matching across both pieces.
Yes. Our in-house CAD technicians and Santoni programming specialists can reverse-engineer sample garments directly. By analyzing needle gauge, yarn denier, weight per square meter (GSM), and stitch structure from a physical reference item, we can build a production-ready machine program and produce initial fit samples within 5–7 days.
Every seamless unit undergoes four strict quality checks: an on-creel optical check for broken filament flaws during knitting, an unrelaxed tubular dimension check, a post-autoclave heat-setting test for colorfastness, and an inspection where garments are stretched over four-way measuring frames to verify recovery percentages and dimensional tolerances.
The standard baseline requires OEKO-TEX Standard 100 (Class 1 or 2), confirming the garment is free from harmful azo compounds, heavy metals, and formaldehyde residues. For US compliance, base layers must meet CPSIA guidelines and ASTM flammability rules. Brands using recycled yarns must also maintain a valid Global Recycled Standard (GRS) Transaction Certificate across the supply chain.
Connect directly with our engineering floor in Istanbul. Share your reference garments, planned colorways, or target tech specifications to receive detailed yarn options, production cost modeling, and rapid sample prototyping within 24 hours.
Santoni Precision Knitting • 1,000 Pcs Flexible MOQ • Worldwide Expedited Logistics