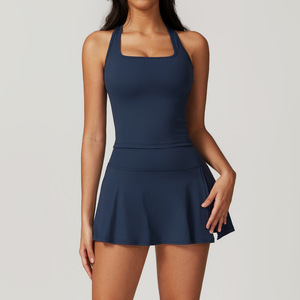
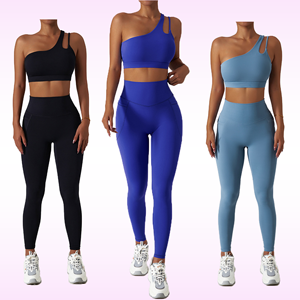
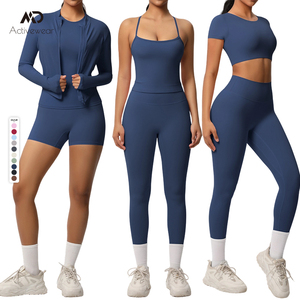
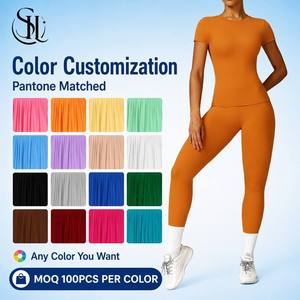
Directly manufactured utilizing high-tensile 4-way stretch fibers, engineered zone compression, and moisture-wicking capillary channels. Available under private label specifications.
Eliminating third-party subcontracting margins and inconsistencies through integrated circular knitting, proprietary yarn preparation, computerized pressure profiling, and certified batch testing.
Our plant houses 20 state-of-the-art Italian Santoni Top2V machines running 28-gauge precision tooling. Seamless cylindrical tubes are synthesized directly from cones, ensuring uniform tension and zero torso side-seams.
Traditional athletic apparel factories require 4 to 6 weeks for initial fit samples. By deploying in-house Lonati & Santoni programming stations, our engineers translate your technical pack or reference garment into knitting code in hours.
Activewear failures stem from seam slippage, grin-through on high extension, and color bleed under perspiration. Every batch undergoes four-tier inspection adhering to strict international sporting standards.
| Performance Parameter | Proprietary In-House Seamless (Santoni Top2V) | Standard Wholesale Cut-and-Sew |
|---|---|---|
| Structural Seam Friction | Zero side seams; integral waist/thigh transitions minimize friction points by 85%. | Multiple overlocked join seams susceptible to chafing during high-cadence motion. |
| Micro-Zoned Thermoregulation | Programmed mesh vents and open-knit lattices knit natively into sweat zones. | Requires piecing separate mesh fabrics together with bulky, rigid flatlock stitches. |
| Yarn Consumption & Fabric Waste | Engineered pre-form tube knitting restricts total fabric cut scrap below 4.5%. | Substantial marker waste (18%–28%) generated during standard pattern cutting. |
| Dimensional Stability & Wash Cycle | Heat-stabilized yarn setting delivers shrink control < 2.5% after 50 industrial washes. | Prone to torque and twisting when warp and weft tensions vary across sewn panels. |
Strategic product directors are transitioning from generic polyester blends to biomimetic composites, circular polyamides, and localized hydrodynamic compression architectures.
Brands are demanding post-industrial and ocean-reclaimed PA6.6 yarn extruded with high molecular integrity. These synthetics mirror virgin fiber strength, providing superior dye intake without crystalline polymer degradation.
Instead of uniform squeeze, modern gym wear demands zoned compression. Using differential elastomeric loop density, garments stabilize pelvic tilt, minimize hamstring oscillation, and facilitate venous return without restricting range of motion.
Moving away from topical wash-off chemical wicking finishes, current innovations integrate channeled micro-groove yarn profiles (e.g., cross-shaped filatures) that pull perspiration mechanically for the complete lifespan of the activewear.
Embedded anti-odor mineral particles at the masterbatch melt stage neutralize volatile organic compounds (VOCs) released by bacterial metabolization of sweat, meeting consumer demands for multi-day wear and sustainable low-temperature laundering.
How leading multi-channel fitness brands mitigate geopolitical tariffs, volatile shipping indices, and inventory bullwhip effects through agile supply alliances.
Long-distance maritime supply chains running 35 to 55 days from Far East hubs expose retailers to seasonal demand mismatches. Utilizing strategic production hubs near European and Atlantic sea-corridors compresses transit to 3–7 business days, radically shrinking holding inventory liabilities.
Modern regulatory directives (EU CSRD, Digital Product Passports) necessitate full traceability from crude chips to finished leggings. Our facilities utilize OEKO-TEX Standard 100 Class I certified dyes and maintain strict zero-discharge hazardous chemical (ZDHC) water management protocols.
Top-tier sportswear operators no longer purchase rigid seasonal stock 9 months in advance. By pre-allocating greige yarn stocks, we enable our corporate partners to operate on agile 1,000-piece rolling commitments, dyeing and branding dynamic colorways based on real-time sell-through metrics.
Direct, transparent answers regarding manufacturing capabilities, minimum volume matrices, testing thresholds, and export logistics.
For fully customized OEM/ODM seamless athletic garments, our baseline run is 1,000 units per style. To empower fast-growing performance brands, we permit this volume to be split across up to 2 distinct sizes and up to 3 pantone-matched colorways (e.g., 500 Medium, 500 Large split into Sage Green, Charcoal, and Midnight Black). For specialized cut-and-sew capsule styles, flexible runs starting at 100 pieces are supported.
Squat opacity is a mechanical equation governed by denier count, air-jet texturing, and needle density. We utilize 70D/24F double-covered high-stretch microfibers coupled with 28-gauge Santoni dial-and-cylinder spacing. This yields a dense, interlocked interlock fabric structure ranging between 280 to 340 GSM that passes 180-degree luminosity opacity bend checks without stiffening hand-feel.
Yes. More than 45% of our international OEM projects originate from an existing benchmark garment. Our textile engineers perform dimensional deconstruction, fiber burn testing, spectrophotometer color matching, and digital stitch density mapping to recreate and optimize the prototype into an industrial manufacturing matrix within 5 to 7 working days.
Upon approval of pre-production counter samples (PPS) and lab dip color sign-offs, industrial knitting, piece-dyeing, silicone heat-transfer branding, and poly-bag packaging typically conclude in 25 to 35 calendar days. Transit times depend on geographical target: air freight to North America and Europe arrives in 3–5 days; regional European road freight arrives within 4–6 days.
We provide comprehensive OEM brand integration: high-elasticity silicone transfer logos (which stretch up to 200% without cracking or adhesive separation), knitted-in jacquard waistbands, ultrasonic laser cut tags, GRS-certified biodegradable zip bags, customized barcode hangtags, and branded moisture-resistant corrugated outer cartons certified for Amazon FBA or central distribution centers.
Every single batch is monitored under strict ISO 9001 and AQL 1.5/2.5 protocols. Before sealing, goods pass needle detector channels, seam-torque measurements under tension, stretch recovery testing, and random perspiration color rub fastness evaluations (Crockmeter wet/dry 4.0+ grade). Digital inspection dossiers are dispatched directly to the buyer's procurement team prior to shipping release.
Bypass intermediary trading agencies. Leverage our in-house Santoni knitting floor, 5-7 day fast prototyping unit, and dedicated technical sales engineers to scale your label's profit margins and operational velocity.