20+
Santoni Top2V Gauge 28 Knitting Units
5-7
Days Rapid Prototyping Cycle
1,000
Pcs Flexible MOQ (Split Options)
25+
Global Sourcing Destinations
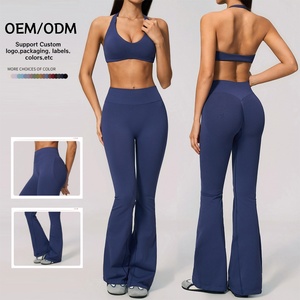
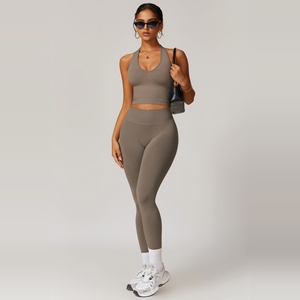
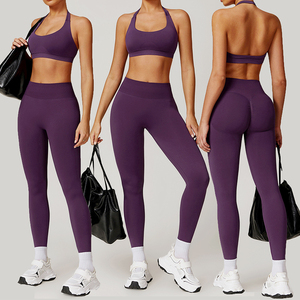
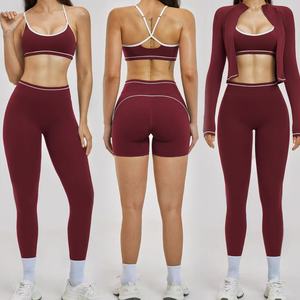
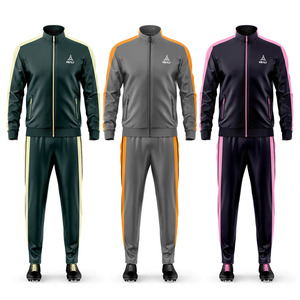
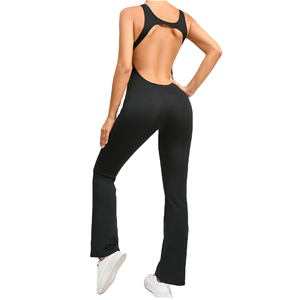
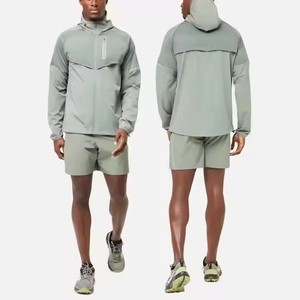
Precision-Engineered Seamless Activewear Silhouettes
Explore our validated product architectures engineered on 28-gauge circular knitting machines, offering zoned compression, zero side-friction, and structural durability.
Why Tier-1 Performance Brands Partner with Our Plant
Vertical in-house knitting, localized European supply corridors, and tight parameter control eliminate third-party subcontractor friction.
Direct Santoni Fleet Control
Unlike trading agencies or cut-and-sew aggregators, we operate 20 specialized Santoni Top2V machines (gauge 28) directly inside our Beylikdüzü, İstanbul facility. This guarantees absolute uniformity across tensile strength, stretch modulus, and circular compression bands.
5-7 Day Prototyping Cycle
By bypassing third-party knitting subcontracts, our in-house machine programmers translate tech packs or sample garments directly into circular stitch files. Complete prototype samples ship in as fast as 5 to 7 operational days for rapid fit testing.
Optimized MOQ Architecture
We respect inventory cash-flow. Our production runs start at a baseline of 1,000 pieces per style, with flexible internal matrix allocations enabling splits across up to 2 sizes and 3 custom colourways (e.g., 500 Medium / 500 Large across distinct color baths).
Squat-Proof Structural Integrity
Microfiber Polyamide 6.6 and Air-Covered Elastane (Lycra®) matrices provide full opacity without excessive garment weight. Every batch undergoes strict stretch-recovery and zero-grinning fabric analysis before assembly.
Strategic Nearshore Transit
Situated in İstanbul, our factory enables door-to-door delivery throughout the European Union in 3 to 7 days by road freight, completely eliminating standard 6-to-8 week container vessel chokeholds from East Asia.
Direct Multi-Lingual Engineering
No intermediaries or lost-in-translation errors. Our senior manufacturing account liaisons provide responsive, real-time technical project coordination in English, Turkish, and Russian, with dedicated coverage for North America.
Engineering Insights: Seamless Activewear Evolution & Procurement Shifts
Data-driven technical analysis for activewear brand directors, supply chain heads, and technical designers navigating modern apparel dynamics.
1. The Mechanical Advantage: Continuous Tubular Knitting Over Cut-and-Sew
Traditional cut-and-sew activewear suffers from structural vulnerabilities: flat fabric panels are drafted, cut, and assembled via flatlock, coverstitch, or overlock seams. This assembly framework causes two persistent failure modes: localized frictional chafe along high-movement meridians (such as inner thighs and axillary borders) and differential seam breakdown under continuous cyclic tension.
In contrast, our Santoni Top2V 28-gauge circular knitting technology produces an anatomically calibrated, seamless tube directly from the raw cone yarn. The machine’s multi-feed computerized control allows selective needle selection, switching from a supportive 3x1 rib waistband to an open-hole diamond ventilation mesh and into a high-density, squat-proof interlock knit—within a single continuous operation. The absence of lateral side seams ensures that elongation modulus remains uninhibited across the circumference of the garment, drastically diminishing shear strain on user skin and boosting product lifecycle durability.
2. Future Activewear Procurement Trends (2025–2030)
Activewear sourcing is departing from monolithic, high-inventory ocean orders toward compressed production sprints driven by three macro currents:
Circular Biodegradable Synthetics
Procurement teams are shifting from standard Polyamide to bio-based Nylon (Castor bean polyamides) and enhanced degradation synthetic yarns (Amni Soul Eco®) that degrade in anaerobic landfills within 3 years without sacrificing tensile modulus.
Hybrid Nearshore Hedging
Supply-chain fragility has forced Western brands to allocate 30-40% of their open-to-buy budgets to European-hub nearshore factories. Shorter turnaround buffers allow mid-season reorders aligned with live customer sell-through rates.
Targeted Functional Compression
Generic high-spandex blends are yielding to targeted, zoned compression. Modern gym consumers demand graduated pressure maps along muscle bellies to assist lymphatic flush, coupled with high-wicking, breathable aeration channels.
Our facility continuously benchmarks yarn developments against these shifts, working directly with master dye laboratories to maintain standard Oeko-Tex® 100 Class I certifications and dynamic colorfastness across recycled polyamides and low-impact dope-dyed yarns.
3. Technical Sourcing Comparison Matrix
When evaluating suppliers for core activewear programs, assessing total-cost-of-ownership (TCO) demands careful trade-off mapping:
| Production Attribute | In-House Santoni Seamless (Our Plant) | Cut-and-Sew Assembly Plants |
|---|---|---|
| Textile Yield & Waste Rate | < 4% (Yarn converted straight to silhouette tube) | 15% - 22% cutting room table scrap loss |
| Abrasion & Skin Shear | Virtually zero; integrated seamless perimeter | Elevated along multi-needle overlock seams |
| Design Iteration Flexibility | Software-controlled needle matrix program updates | Physical re-patterning, cutting die adjustments |
| European Transit Speed | 3 to 7 Days via direct ground freight | 35 to 55 Days via deep-sea cargo routing |
Frequently Asked OEM/ODM Sourcing Questions
Direct technical answers addressing engineering capabilities, order mechanics, and production workflows.
Are you an authentic physical manufacturer or a trading export intermediary?
We are a dedicated, vertically integrated manufacturing factory. We engineer machine software, procure filament yarns, operate 20 in-house Santoni Top2V circular knitting machines in Beylikdüzü, İstanbul, and manage piece-by-piece final garment finishing. We do not sell clearance stock or broker third-party output—every piece is produced directly for your private label.
What is the standard Minimum Order Quantity (MOQ) and size breakdown flexibility?
Our standard production threshold is 1,000 units per individual style. To support scalable SKU rollouts, we allow this baseline order of 1,000 pieces to be divided across up to 2 size tiers (e.g., 500 Small/Medium and 500 Large/XL) and distributed across up to 3 custom lab-dipped Pantone shades.
How does the sampling turnaround run in 5 to 7 days?
Because technical CAD design and machine programming occur directly on the factory floor, there are zero third-party handoffs. Once your tech pack or benchmark physical garment arrives, our certified Santoni technicians convert stitch requirements into code, thread machine creels, and run prototype tubes within 5 to 7 working days.
What customization options are offered under full-package OEM/ODM terms?
Full-package options cover jacquard-knitted logos, localized engineered textures (ribbed, micro-mesh, honeycomb), heat-transfer silicone badging, custom silicone grip waistbands, OEKO-TEX woven care labels, eco-friendly hangtags, and individualized branded polybags.
How does Turkish production improve import duty profiles in Europe and North America?
Under the EU–Turkey Customs Union, manufactured textile goods shipped from Turkey typically benefit from zero-tariff treatment into European Union states via A.TR movement certificates. For the United States, our streamlined logistics connections via major air and sea terminals in İstanbul ensure transparent, predictable customs processing.
Start Engineering Your Next Seamless Activewear Line
Provide your tech pack, physical sample references, or target fabric specs. Our factory engineering team will furnish yarn breakdowns, program feasibility assessments, and unit pricing within 24 hours.
Low 1,000 pc MOQ · 5-7 Day Prototyping · Direct Factory Pricing