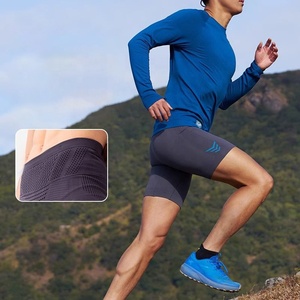
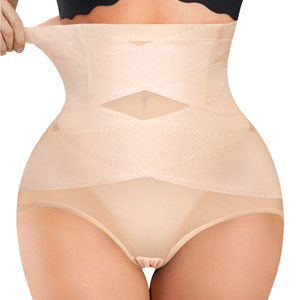
Explore our turnkey OEM line engineered with body-contouring zones, quick-dry microfibers, and zero chafe construction.
A systematic breakdown of circular mechanical engineering, yarn dynamics, and production agility for technical activewear procurement officers.
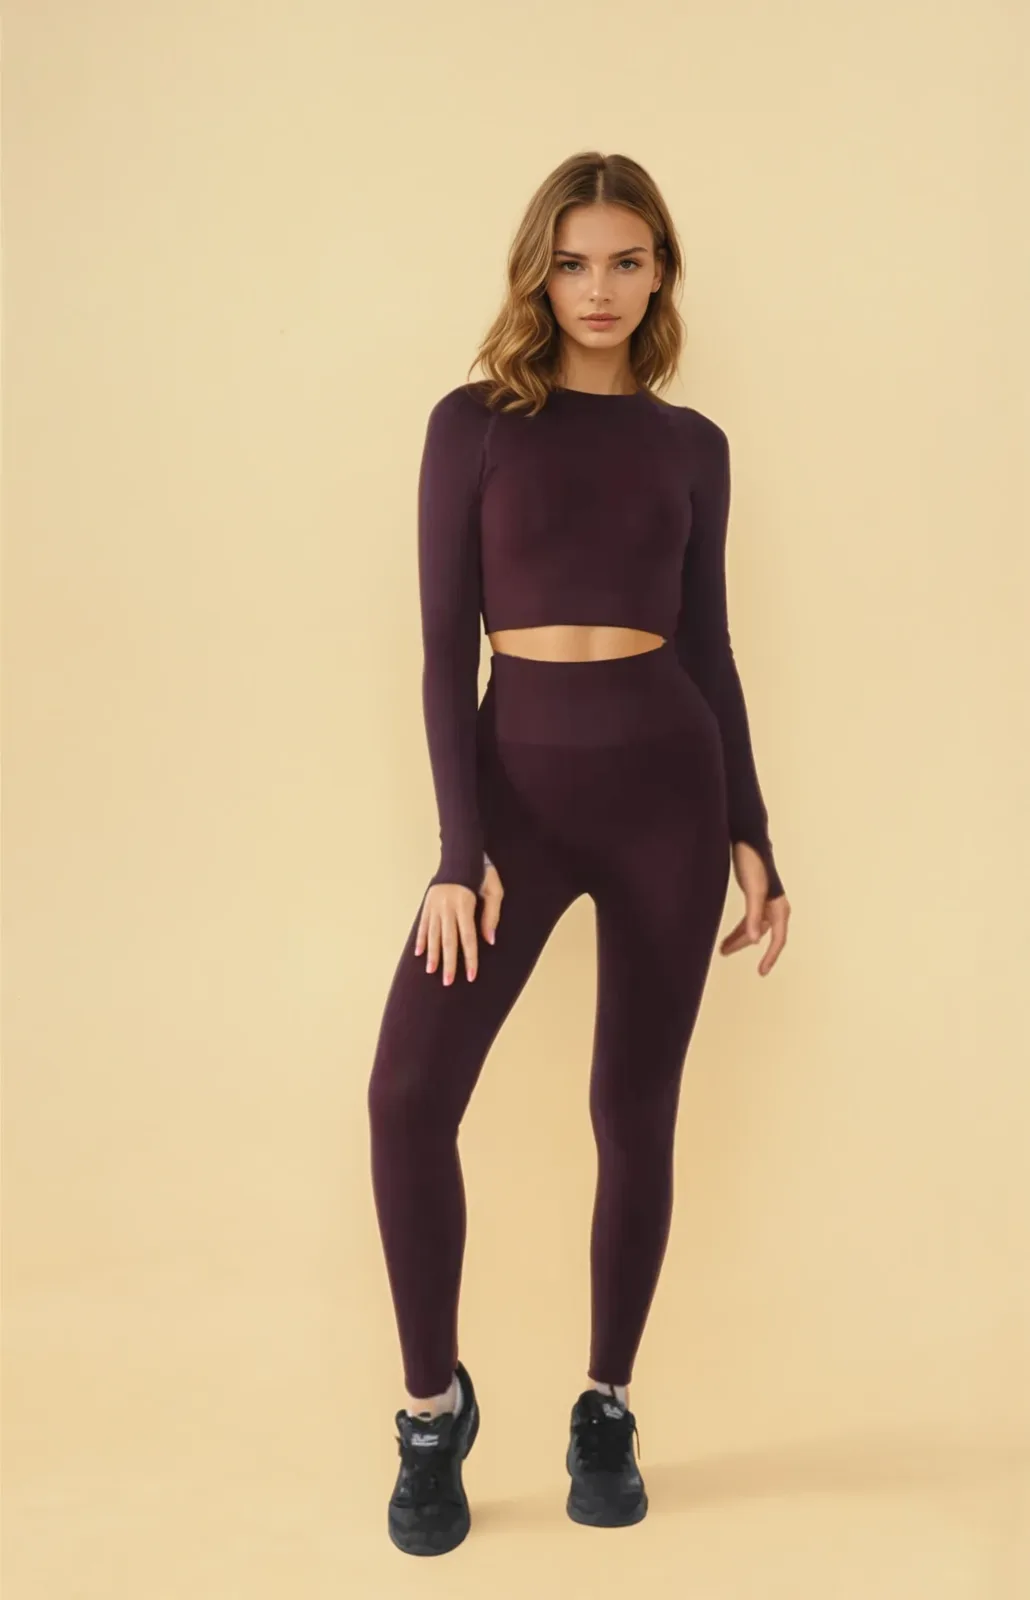
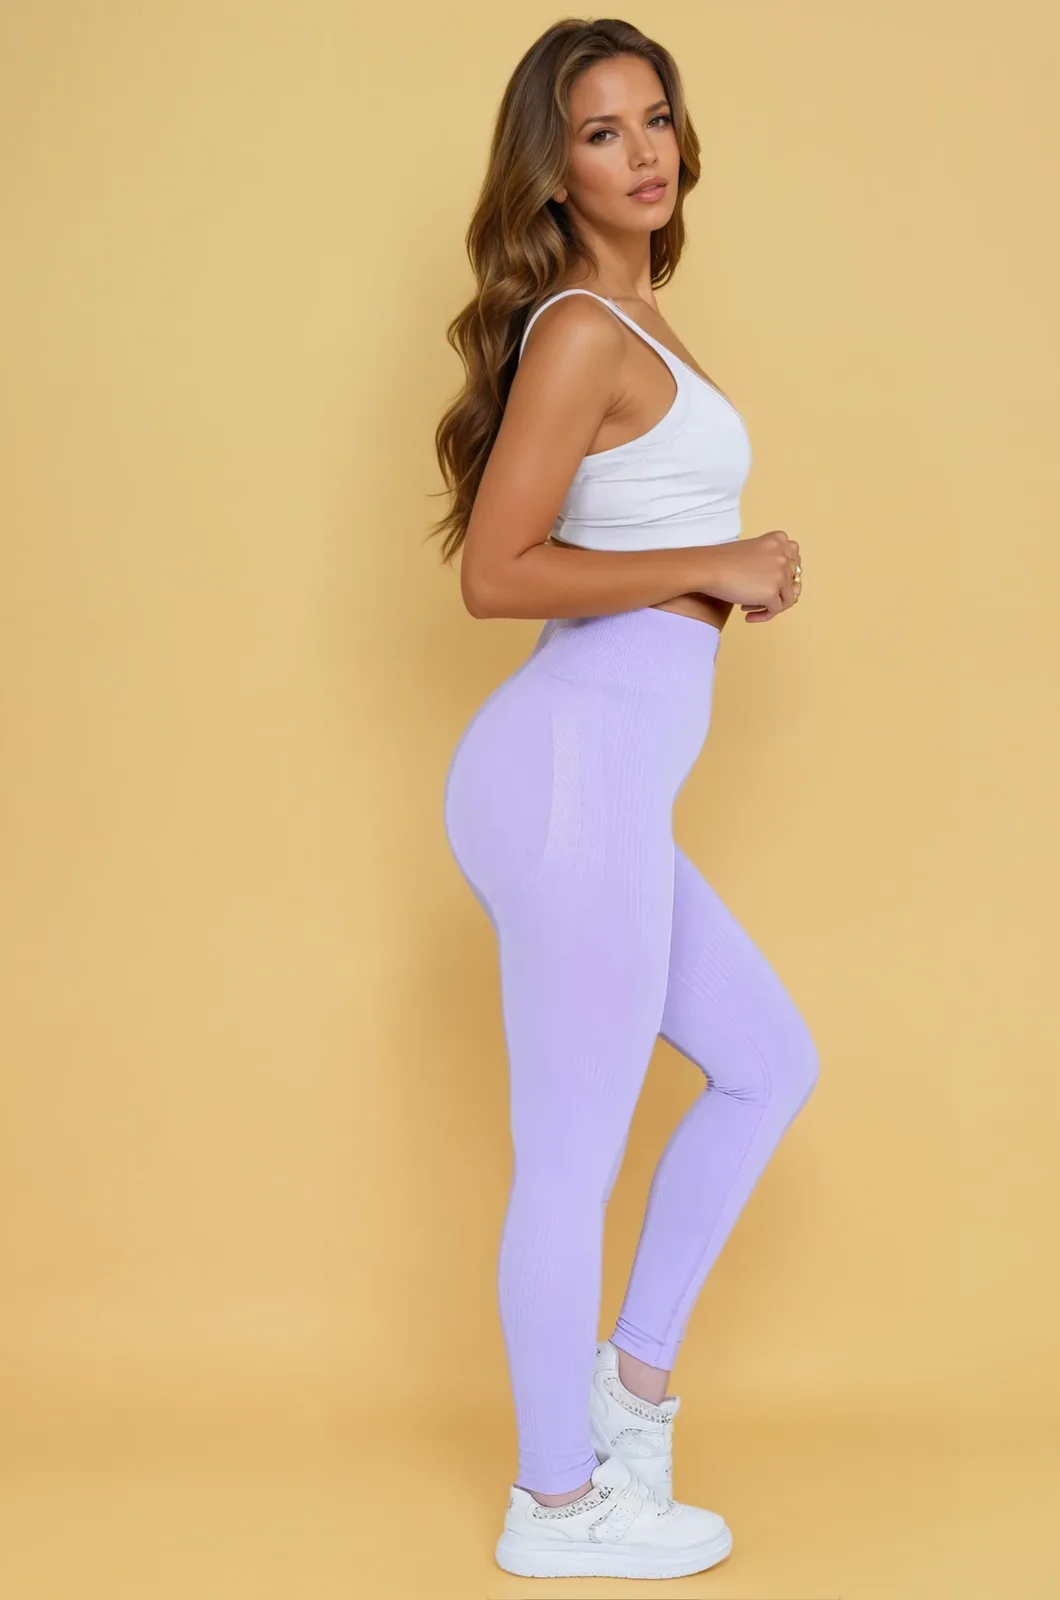
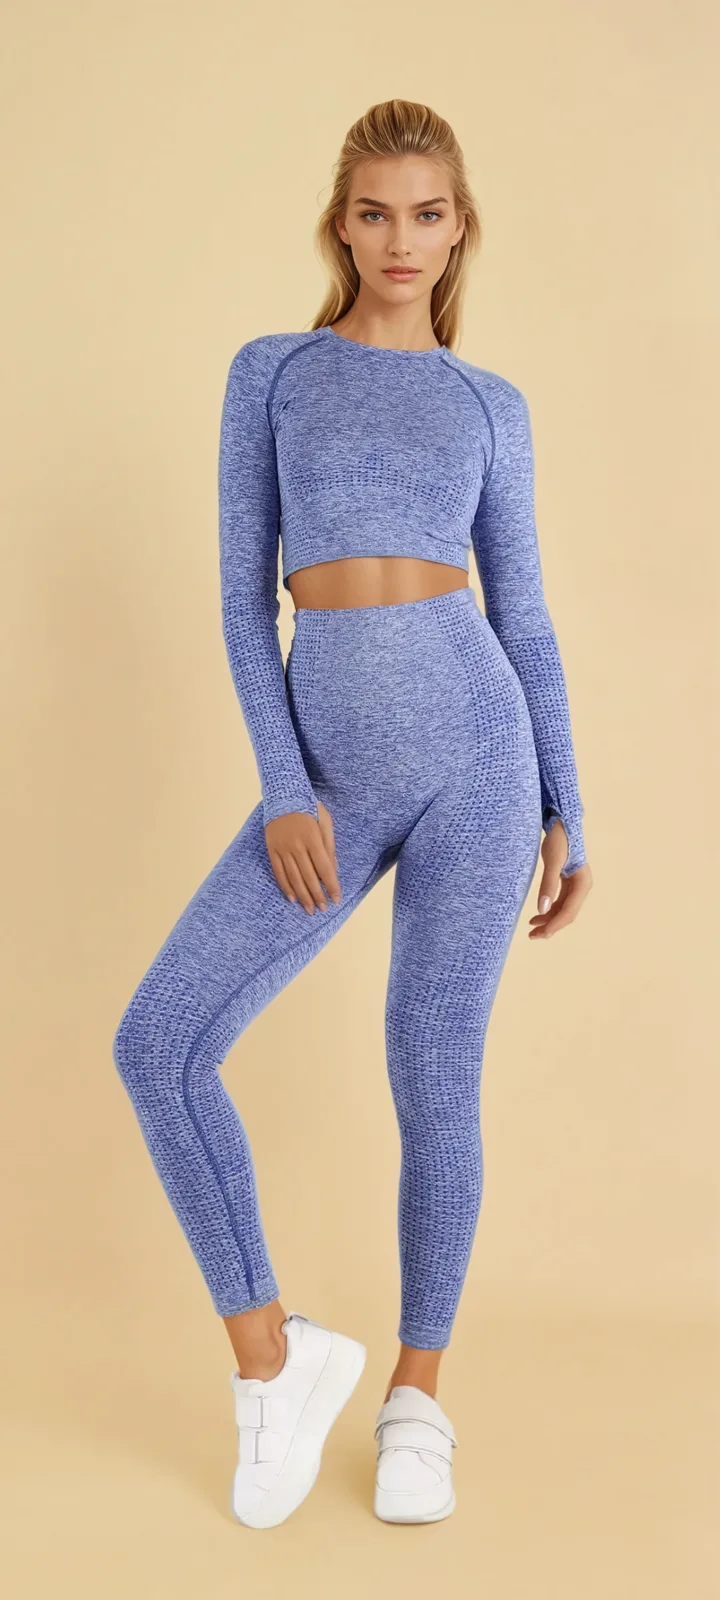
Traditional athletic wear stitches multiple cuts of fabric together, producing bulky seams that cause chafing under athletic duress. In contrast, our Santoni circular knitting machines (Gauge 28) program multi-density micro-mesh channels, rib compression bands, and breathable eyelets within a single continuous tubular piece. This eliminates lateral friction, maximizes tensile durability, and ensures uniform tension across movement cycles.
The performance profile of seamless workout sets depends fundamentally on yarn denier and covering techniques. We utilize Air-Covered Yarn (ACY) pairing Polyamide 6.6 with high-modulus Spandex (such as Roica or Creora) to achieve squat-proof opacity at 280–350 GSM without excess bulk. Polyamide 6.6 provides superior moisture transport rates, rapid thermal dissipation, and long-term pill resistance compared to conventional polyester.
Conventional cut-and-sew garment lines lose roughly 15% to 22% of raw material during pattern nesting and marker cutouts. Seamless tubular knitting consumes yarn strictly required for each garment silhouette, dropping offcut fabric loss below 2%. For ESG-mandated global brands, switching to seamless circular knit technology reduces baseline carbon footprints and speeds scrap mitigation protocols.
| Performance Metrics | Seamless Santoni Circular Knit (28G) | Cut-and-Sew Flatlock Activewear | Procurement Advantage |
|---|---|---|---|
| Skin Surface Friction | Near Zero Tubular, single-piece knit | Moderate to High (Multiple flatlock seams) | Higher consumer satisfaction, lower return rates |
| Targeted Compression Zones | Programmed digitally in-cylinder per zone | Requires cut-in elastane panels & bonding | Eliminates delamination risk and extra cut costs |
| Fabric Scrap Rate | < 2.5% per production batch | 16.0% – 22.0% during pattern nesting | Direct reduction in landed material costs |
| Prototyping Cycle | 5–7 Days (In-house code adjustment) | 14–21 Days (Pattern grading & fabric milling) | Immediate market reaction to micro-trends |
How international fashion-athletic brands are navigating nearshoring, bio-synthetic inputs, and inventory velocity.
Supply chain shocks over the past five years have driven apparel brands to shorten supply lines. Sourcing out of hubs like İstanbul, Türkiye provides unmatched logistics speed for Western Europe and North America. European retailers receive road freight shipments in 3 to 5 days, avoiding lengthy 35-to-45 day container voyages across maritime choke points and reducing working-capital exposure.
Global demand is shifting quickly toward GRS-certified recycled Nylon 6, Seaqual marine polymers, and dope-dyed filaments. Dope-dyeing introduces pigment straight into the polymer melt phase before extrusion, slashing water and chemical usage by up to 80% compared to piece dyeing. Forward-looking OEM workout set collections now integrate biodegradable elastanes to achieve true circularity.
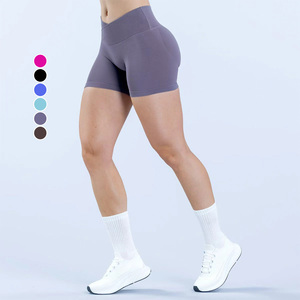
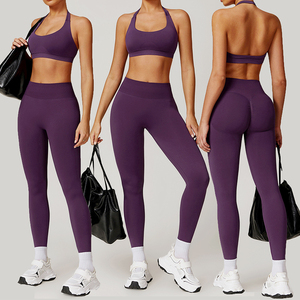
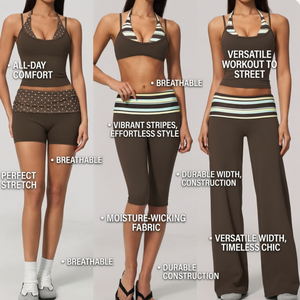
Workout wear is no longer confined to the gym floor. Market data shows accelerated buyer preference for hybrid activewear: ribbed seamless crop tops matched with fold-over flare pants, halter sports bras, and sculpted bike shorts that transition seamlessly into everyday casual styling. Modern OEM designs feature matte luxury finishes and tailored contour accents rather than generic high-shine sportswear aesthetics.
In-house Santoni Top2V production delivering uniform tension, zero color variance, and hand-inspected finishing.
Eliminate intermediary trade markups by collaborating straight with our technical knitting engineers and sampling workshop.
We are a true primary manufacturer, not a sourcing broker. In our Beylikdüzü, İstanbul facility, our battery of 28-gauge Santoni Top2V circular knitters operates under strict humidity- and temperature-controlled conditions. This setup ensures our knits never suffer from cross-batch elastic degradation, uneven needle strikes, or tension deviations.
Because code programming, yarn stocking, and cylinder adjustments all take place on our own factory floor, your tech pack or reference sample moves from digital pattern into a wearable prototype in as little as 5 to 7 business days. This allows creative teams to finalize fit reviews and pre-sell collections well ahead of typical seasonal deadlines.
We combine scalable factory output with adaptable minimums: our standard run is just 1,000 pieces per style. You can split this across up to 2 sizes and up to 3 custom colorways (such as 500 Medium and 500 Large across complementary color pairings). This lowers upfront inventory risk while maintaining healthy wholesale margins.
Clear, direct specifications covering order mechanics, fabric testing, sizing tolerances, and private-label packaging.
We are a dedicated seamless knitwear manufacturer located in Beylikdüzü, İstanbul, Türkiye. Every garment is knitted in shape on our 20 in-house Santoni Top2V machines. We select, inspect, and purchase raw yarns directly, manage the digital cylinder programming, and supervise dyeing and heat-setting alongside vetted finishing mills. You work directly with our engineering and floor operations team.
Our standard MOQ is 1,000 units per style. Within that 1,000-unit batch, we offer brand-friendly flexibility: you can split the order across up to 2 sizes and 3 colors (for example, 500 in size Small and 500 in size Medium divided among 2 or 3 Pantone selections). Additional silhouettes require their own 1,000-piece production setups due to cylinder changeovers.
Fit samples, strike-offs, and jacquard verification prototypes take approximately 5 to 7 working days once yarn specifications and artwork are approved. Following sample sign-off and lab dip clearance, full bulk production typically ships within 30 to 45 business days, depending on overall volume and packaging requirements.
We calibrate our 28-gauge needles to a dense 300–350 GSM fabric yield, combining high-filament Polyamide 6.6 with double-covered Spandex threads. Every prototype is subjected to standardized multi-directional stretch and squat-opacity testing in our QC lab to ensure zero see-through or elastane "grinning" during deep-movement workouts.
We provide full-spectrum OEM finishing: knitted-in jacquard logos, reflective heat-transfer branding, sonic-welded rubber badges, woven inner labels, custom silicone grip strips, customized FSC hangtags, and 100% biodegradable zipper polybags printed to your brand standards.
Located in İstanbul at the intersection of Europe and Asia, orders to major European logistics hubs can arrive within 3 to 7 days via road or express air freight, with duty-free treatment under the EU Customs Union. For North American customers, direct air connections and consolidated sea shipping out of Ambarlı Port keep port-to-door transit times fast and dependable.
Share your digital tech packs or target reference garments. Our engineering team will review your specifications and deliver yarn options, structural knitting breakdowns, and a verified sampling schedule.