Engineered stitch-by-stitch on Santoni circular knitting machinery for anatomical shaping, targeted graduation, and squattable athletic density.
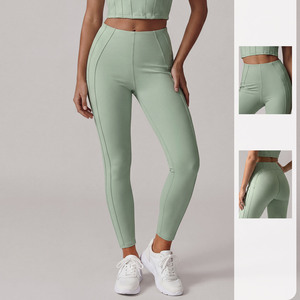
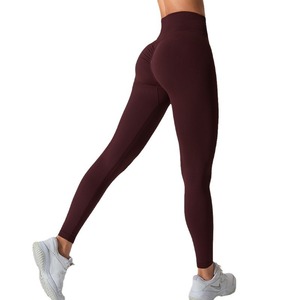
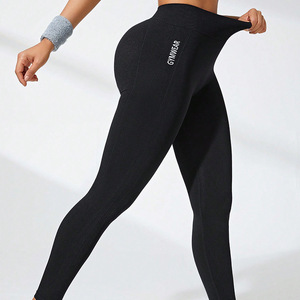
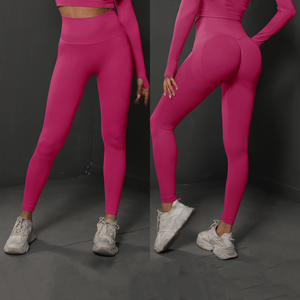
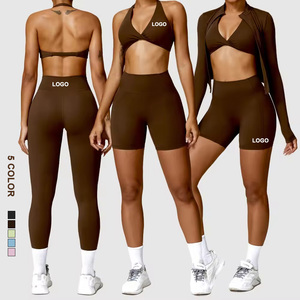
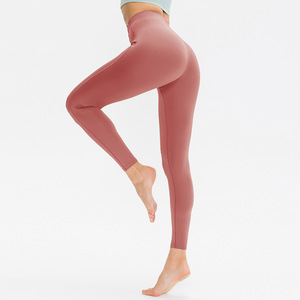
Why Tier-1 athletic labels and independent brands bypass standard brokers to knit directly on our proprietary circular floor.
We do not broker or subcontract tube production. Operating 20 original Italian Santoni circular knitting machines (Gauge 28), our computerized systems map graduated micro-mesh ventilation and heavy compression bands directly into a seamless cylinder.
Eliminate typical 6-week sampling queues. Because pattern programming, yarn creeling, and seamless tube execution happen under one roof, digital tech-packs transition into real physical counter-samples within 5 to 7 operational days.
We combine industrial capability with brand agility. Our structured 1,000-piece baseline per style allows commercial split testing across up to 2 anatomical sizes and 3 bespoke lab-dipped pantone colorways, mitigating inventory overhang.
Color fastness and stretch elasticity are managed through dedicated partner mills under strict inspection protocols. We verify zero torque twist, minimal shrinkage rates (<3%), and consistent tension before final cutting, bar-tacking, and packaging.
Serving wholesale partners across 25+ countries in North America, Western Europe, and Australasia. Dedicated sales engineering units provide documentation in fluent English, Turkish, and Russian, ensuring streamlined customs clearances and DDP logistics.
From silicone anti-slip inner waistbands and woven loop tags to custom heat-transfer reflective branding and eco-friendly compostable polybags, we supply ready-for-shelf SKU packaging engineered for direct retail and D2C warehouse distribution.
A granular side-by-side analysis of why seamless circular knitting outperforms conventional cut-and-sew apparel in athletic tights manufacturing.
| Performance Metrics | Seamless Circular Knitting (Santoni Top2V) | Traditional Flat Cut-and-Sew |
|---|---|---|
| Structural Integrity | Continuous tubular knit; zero longitudinal side seams to burst under lateral load. | Multi-panel overlock flatlock seams; prone to thread breakage at high stress. |
| Fabric Waste Factor | Under 5% (Knitted to specified cylinder shape; raw yarn efficiency). | 18% – 24% (High fabric scrap generation during pattern layout & cutting). |
| Zoned Compression | Dynamic variable tension programmed via knit jacquard; zero bulky inserts. | Requires secondary compression panels sewn together, adding internal friction. |
| Skin Friction Index | Ultra-low skin abrasion index; completely flush interior knit face. | Substantial chafing risk along inner thighs and hips caused by raised stitches. |
| Tensile Elastic Recovery | Multi-directional 360° stretch with air-covered Spandex yarns (Elasthane). | Bi-directional stretch restricted by longitudinal seam rigidity and stretch limits. |
The global seamless activewear market is transforming. Key shifts international buyers must integrate into their upcoming bulk inventory cycles.
Global demand is migrating rapidly from virgin fossil synthetics to GRS-certified Recycled Nylon 6.6 (Polyamide) and bio-derived polyamides. Major European and North American buyers are prioritizing zero-carbon yarns with traceable supply chain pedigree to satisfy stricter regulatory standards.
Physical compression is no longer enough. Forward-thinking procurement managers are specifying antimicrobial silver-ion infusions, Phase Change Materials (PCM) for dynamic thermoregulation, and non-toxic zinc-pyrithione moisture treatments embedded into the core polymer before extrusion.
Wholesale clients are transitioning away from high-risk semi-annual massive bookings toward responsive rolling monthly drops. Factories with integrated programming, in-house knitting, and responsive greige yarn storage allow brands to react instantly to viral social trends.
A closer look at how machine learning programming and ultra-fine gauge machinery are redefining activewear manufacturing standards.
While traditional seamless tights run on 28-gauge cylinders, modern production floor upgrades now introduce 32-gauge and 36-gauge Santoni configurations. This enables an ultra-light, buttery naked handfeel while achieving absolute 100% opacity, completely passing strenuous squat tests without increasing garment weight.
Early seamless activewear suffered from elastane grin-through and premature sagging after repeated wash cycles. By utilizing air-jet covered dual filament Lycra cores wrapped in textured nylon microfibers, our tights exhibit instant recovery resilience exceeding 96% retention after 100 industrial wash cycles.
Knitting programs have transitioned from primitive ribbed structures to multi-layered topographical compression zones. Algorithmic stitch distribution concentrates firmer denier knits across the lower abdomen, lumbar back, and sub-gluteal fold while simultaneously opening porous venting holes across the knee and calf.
Essential trade details covering technical capabilities, minimums, logistics, and quality assurance for commercial wholesale buyers.
Our standard production MOQ is 1,000 pieces per style. Within this 1,000-piece production run, we allow splits across up to 2 sizes (e.g., 500 S/M and 500 L/XL) and up to 3 customized pantone colorways. Custom lab dip matching is included.
Opacity in seamless tights is governed by yarn denier selection, stitch loop density, and gauge calibration. We employ high Dtex textured nylon combined with dual air-covered spandex knit structures, tested under calibrated 2,000-lux stretch lighting to verify zero sheer visibility.
Yes. If you do not possess a formal tech pack, you can send us a physical benchmark garment. Our in-house textile engineers will deconstruct the yarn composition, measure loop density, decode the circular machine pattern, and produce a counter-sample within 5 to 7 days.
We supply full OEM/ODM customization: seamless knitted jacquard logos, high-elastic heat transfer prints (matte, reflective, silicone), inner silicone grip bands, custom silicone or rubber badges, branded woven wash labels, and custom biodegradable retail packaging.
Prototyping and lab dip approvals require 5–7 working days. Once the pre-production sample (PPS) is confirmed and the deposit is secured, mass circular knitting, piece dyeing, bar-tacking, and quality control typically take 25 to 35 working days depending on total order volume.
Every single seamless piece undergoes a 4-step inspection regimen: inline grey-cloth tube inspection for dropped stitches, post-dyeing color-shade continuity inspection under standard D65 illuminants, 4-way tensile stress testing, and final hand measurements against the approved spec sheet.