Explore our core OEM production capabilities. Utilizing continuous circular Santoni programming, multi-feed microfilament nylon yarn, and bonded elastication, our manufacturing line delivers ultra-resilient performance activewear tailored to high-tier brand catalogs.
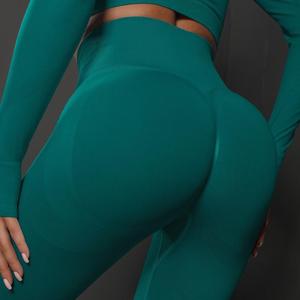
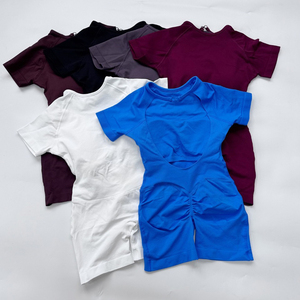
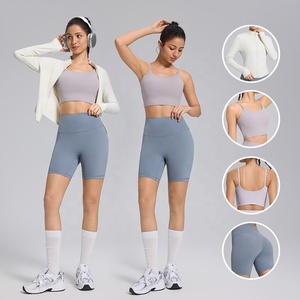
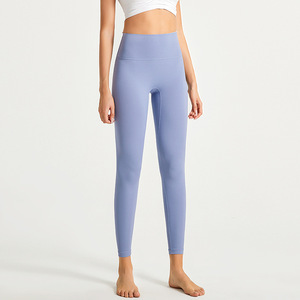
The manufacturing architecture of commercial biker shorts and technical tights has transitioned entirely away from conventional cut-and-sew operations. In high-efficiency export facilities, the transition to computer-aided circular knitting machines (primarily Santoni Top2V Series, Gauge 28) enables the unified generation of targeted compression, heat dissipation channels, and structural waist ribbing directly from raw yarn bobbins without longitudinal side seams.
When engineering premium wholesale biker shorts, thermal regulation is calibrated via stitch-mesh variation across the lumbar spine and lower pelvis. By manipulating feeding tension across 4-ply core-spun Polyamide 6.6 mixed with bare elastane (ranging between 20D to 70D), factories eliminate rolling waistbands, sheer transparency under full flexion, and crotch blowout without relying on heavy internal elastic bands.
A definitive production comparison for textile directors, technical designers, and international supply chain leaders.
| Production Dimension | Circular Seamless Tubular Technology | Conventional Cut-and-Sew Processing | Strategic Brand Value |
|---|---|---|---|
| Structural Seams | Zero lateral seams; single inner-thigh flatlock gusset | Dual side seams, waistband topstitch, leg hem lock | Eliminates chafing; delivers second-skin ergonomic contour |
| Variable Compression | Programmed stitch density alters PSI along the quadriceps | Requires differential fabric panels sewn together | Streamlined aesthetics with targeted muscle stabilization |
| Material Yield Efficiency | Under 4% yarn cutting waste per knitted piece | 16% to 24% fabric waste left on spreading markers | Superior ESG compliance and lower raw material overhead |
| Elastic Fatigue Life | Covered microfilament yarns prevent elastane degradation | Overlocked thread tension causes localized fraying | Retains shape and recovery after 100+ commercial wash tests |
| Tooling & Setup Speed | CAD software script uploads directly to circular needles | Requires physical pattern grading, markers, and die cut plates | Rapid prototyping: verified counter-samples ready in 5–7 days |
Market intelligence derived from consumer shift analytics, athletic wear retailer forecasts, and performance yarn developments.
European and North American regulatory pressures (such as the EU Ecodesign Directive) are accelerating the demand for post-industrial and ocean-waste recycled nylon (GRS-certified Nylon 6). Procurement directors are moving away from virgin synthetics toward bio-based feedstocks derived from non-food castor beans that guarantee equivalent tactile elongation without petroleum dependence.
The next iteration of biker shorts bridges sportswear with active skin therapies. Yarns integrated with far-infrared (FIR) emitting minerals bounce back endogenous kinetic energy, boosting muscle recovery times. Simultaneously, zinc-pyrithione or silver-ion microscopic encasements permanently bonded during filament spinning deliver life-of-garment anti-microbial defenses without odor build-up.
Supply chain security is prioritizing decentralized flexibility. Rather than holding 50,000 units in central warehouses, athletic labels partner with manufacturers capable of low-MOQ repeat batching (1,000 pcs per style across 2 sizes and 3 colors). Factory-level digital warehousing allows greige fabric cylinders to sit un-dyed until weekly digital retail sales figures dictate precise piece-dyeing color runs.
Key design iterations distinguishing high-margin performance shorts from generic lifestyle apparel.
Traditional flat stitching flattens posterior anatomy under dynamic load. Next-generation seamless engineering utilizes localized needle dropouts and diamond knit geometry beneath the gluteal fold, providing passive structural lift while relaxing compression across the upper crest to deliver natural definition without uncomfortable scrunch cord lines.
The leading complaint among active consumers is waistband slippage during high-cadence cycling or deep squats. Modern manufacturing employs double-ply Santoni folded edges, blending elastane with variable tension yarn feeding (35 cN down to 18 cN) across the upper rib, creating an organic anatomical lock against the iliac crest without constricting internal organs.
Consumers now require functional device storage even on minimalist activewear. By introducing secondary feeder systems, our automated needles drop drop-pocket compartments directly into the lateral knit matrix, maintaining zero-bulge stability during movement. Pocket edges and gusset joins feature ultrasonic laser-welded seams rather than bulky thread overlocks.
Direct from our precision knitting floor to global retail shelves: eliminating intermediary costs, guaranteeing QA consistency, and delivering exceptional speed to market.
Our facility houses an extensive assembly of in-house Santoni Top2V high-gauge circular knitting machines (gauge 28). We retain 100% direct control over software programming, needle sequencing, and cylinder tensioning without outsourcing core production to unregulated subcontractors.
Speed to market defines apparel profitability. Because CAD programming and sample-knitting run on dedicated in-house pilot lines, our engineering team converts physical reference samples or tech packs into tactile counter-samples in just 5–7 working days for rapid fit reviews.
From custom silicone-transfer brand logos and heat-sealed interior care details to Jacquard knit waistband branding, custom-dyed pantone hues, and recycled retail hang packaging, we deliver fully customized retail-ready collections crafted for direct Amazon FBA or DTC shipping.
We eliminate extreme capital requirements for growing premium activewear labels. Our baseline commercial MOQ is set at 1,000 pieces per style, conveniently split across up to 2 distinct sizes and up to 3 individual colorways (e.g., 500 Medium / 500 Large divided across 2 shades).
Actionable parameters and testing standards essential for quality assurance directors before approving container bill of ladings.
Always mandate an AATCC-verified squat opacity test. Garment fabric must be placed over an illuminated contrast checkerboard under 1,000 lux illumination at 80% maximum bidirectional elongation. True high-performance wholesale biker shorts must show zero luminous show-through at the gluteal apex.
Request dynamic cyclic extension data (ASTM D4964). Premium high-gauge nylon-elastane formulations must document recovery metrics exceeding 92% after 300 sequential cycles at 50% strain. Inferior polyester-heavy alternatives exhibit permanent bagging around the lower knee bands and waist roll down.
Because biker shorts experience heavy mechanical friction combined with acidic perspiration, verify ISO 105-E04 (perspiration fastness) and ISO 105-X12 (crock fastness). Ratings must achieve Grade 4.0 or higher to prevent wet migration onto athletic tops, car seats, or fitness upholstery.
Clear, direct answers regarding production logistics, technical parameters, and export procedures.
We are a certified original equipment manufacturer (OEM/ODM). We directly program, knit, inspect, and finish garments on our own Santoni circular equipment. We manage custom yarn sourcing, software patterning, cutting, flatlock assembly, and export packaging directly from our modern manufacturing floor. You work directly with technical production engineers rather than commission agents.
Our standard production baseline is 1,000 pieces per style. Within that 1,000-piece production allocation, clients can configure up to 2 distinct sizing tiers and up to 3 individual colorways (for example: 500 units in size S/M and 500 units in size L/XL, divided across Black, Navy, and Terracotta). This allows emerging brands to assemble versatile collections without excessive initial inventory risk.
Once design tech packs or reference target garments along with pantone swatches are finalized, functional seamless counter-samples are produced within 5 to 7 business days. Because circular needle programming is executed internally without waiting on external subcontractors, fit corrections and compression refinements are performed immediately on our machines.
Yes. Producing harmonized two-piece activewear sets (combining biker shorts with matching sports bras, crop tops, or jackets) is one of our key specializations. We utilize the exact same yarn dye-lot formulations and calibrate machine gauge densities across both garments, ensuring identical surface luster, tensile hand-feel, and absolute color matching across the entire collection run.
We provide full-spectrum turnkey private-label solutions. This encompasses elastomeric reflective transfer logos, knitted-in jacquard branding along waistlines, custom woven or heat-pressed interior care labels, branded hangtags, biodegradable frosted ziplock retail pouches, and barcoded cartons configured for Amazon FBA or enterprise distribution center intake.
We routinely export to major retail hubs across North America, the European Union, the United Kingdom, Australia, and East Asia. We accommodate standard Incoterms including EXW, FOB, CIF, and DDP (Delivered Duty Paid), offering end-to-end maritime container shipping, expedited air freight, and full customs documentation support directly to your designated warehouse.
Partner with an industry-leading OEM seamless manufacturer. Submit your tech pack, physical sample references, or project volume requirements to receive comprehensive fabric swatches, technical yarn proposals, and an all-inclusive FOB/DDP quotation.
Inquire Now