Seamless Tech
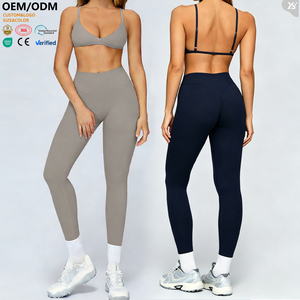
Explore our precision-milled private-label activewear lineup. Every unit is engineered with 4-way mechanical recovery, zone-targeted moisture dispersion, and compression ergonomics.
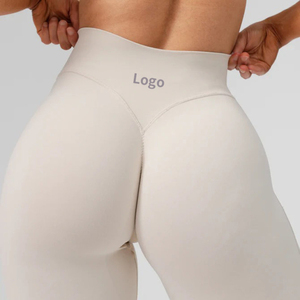
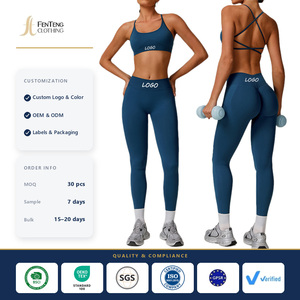
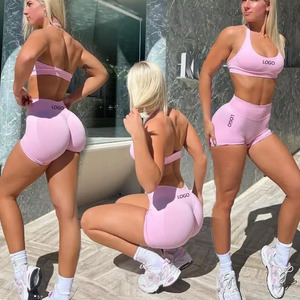
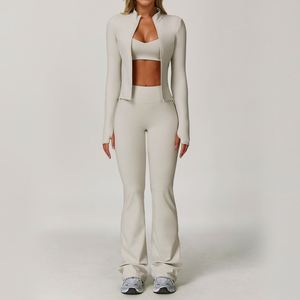
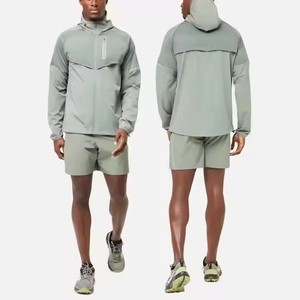
Modern athletic wear procurement is governed by technical precision. Traditional cut-and-sew manufacturing relies on multi-panel stitching where shears slice through knitted sheets, leaving 18% to 24% fabric waste and forming structural stress points that cause skin chafing and stitch blowouts under high tensile load.
By leveraging advanced computerized circular machines—specifically utilizing Santoni Top2V Gauge 28 tubular machinery—our factories synthesize the garment's anatomical architecture directly from high-filament draw-textured yarn (DTY). Micro-mesh cooling zones, muscular stabilization bands, and high-recovery compressive bands are integrated into a continuous, singular yarn matrix.
Supply Chain Information Gain: Circular knitting slashes scrap material to below 1.5%, streamlines flatlock assembly overhead by 62%, and eliminates bulk margins along the hips and lateral torso—yielding unmatched aesthetic streamlining for mid-to-high luxury fitness brands.
From custom air-jet texturing to computerized drop-needle programming, our facilities maintain strict tolerance thresholds over elasticity hysteresis, post-laundering dimensional stability, and delta-E spectrophotometric shade matching.
Verticalized supply integration under one roof: From polymer yarn compounding to automated laser framing, eliminate trading intermediary markups and protect intellectual assets.
We do not broker your orders. Precision seamless knitting is executed 100% on dedicated Santoni circular lines (Gauge 28) for uniform dimensional tension across bulk SKU iterations.
Turn technical tech packs, CAD sketches, or physical benchmarks into fully graded, wearable pre-production samples in 5 to 7 business days, shortening go-to-market cycles significantly.
Our baseline begins at 1,000 units per style with flexible sub-allocation: up to 2 distinct sizes and 3 custom lab-dip Pantone colorways (e.g., 500 Medium & 500 Large across palette variants).
Complete end-to-end white-glove custom identity execution: thermal transfer inner care labels, jacquard-woven elastic waistbands, silicone 3D badges, bio-degradable frosted zip pouches, and retail barcode hangtags.
Stay ahead of category disruptions. Review the technical innovations, circular economy standards, and procurement behaviors defining the next generation of performance apparel.
Virgin nylon dominance is waning. Global retail buyers are pivoting swiftly toward post-industrial recycled Nylon 6.6 (Q-NOVA, ECONYL) and bio-synthesized castor bean polymers that achieve identical tensile elongation without fossil depletion.
The convergence of seamless tubular knitting with ultrasonic edge welding eliminates traditional hem folds. Laser-perforated aeration patterns replace sewn mesh inserts, lowering drag coefficients and delivering superior structural featherweight feel.
Direct-to-consumer athletic brands require garments with variable compression profiles: lower compression around the diaphragm for respiratory ease, paired with high-gauge core and hamstring support to maximize silhouette definition.
The era of rigid 10,000-unit minimums is obsolete. Leading performance brands operate a test-and-reorder model: deploying 1,000 to 1,500 units per colorway across TikTok Shop and Meta ads, backed by pre-reserved greige tubes for fast-turn garment dyeing.
Clear, authoritative technical answers covering minimum order quantities, yarn composition, quality audits, compliance, and international freight logistics.
We are a full-scale direct manufacturer. All seamless circular knitting operations run directly on our in-house Santoni Top2V machines. We purchase certified raw yarns, control in-house circular programming, coordinate dyeing through licensed continuous mills, and oversee cut, sew, iron, and final packaging under our own roof. Clients avoid hidden agency commissions and communicate directly with technical production engineers.
Our standard production run starts at 1,000 units per style. To help you balance your sizing curve and test the market effectively, that 1,000-piece commitment can be split across up to 2 distinct sizes (e.g., S/M and L/XL) and up to 3 separate lab-dipped Pantone colorways. Custom yarn blends or specialized jacquard mesh developments maintain their own dedicated batch runs.
Because all Santoni programming and circular knitting machines operate in-house rather than being outsourced, physical initial strike-off samples are typically completed within 5 to 7 business days from digital tech-pack approval. Once the fit sample is reviewed and signed off, mass production typically completes within 25 to 35 business days depending on order volume.
Squat opacity requires balanced machine configuration and yarn density. We configure circular knit density between 300 to 340 GSM using fine-filament draw-textured nylon combined with double-covered Spandex (Lycra). This dual-filament shielding prevents white elastane grin-through under maximum biomechanical extension, verified through lux-meter light transmission and strict elongation testing.
We enforce strict AQL 2.5 (Acceptable Quality Limit) standards on every production run. Our quality inspectors conduct in-line 4-point fabric audits, verify seam tensile shear resistance on digital push-pull gauges, check flatlock seam integrity, and perform colorfastness tests against perspiration and rub-wear. Independent third-party inspection firms such as SGS, Intertek, or TÜV are welcomed on site.
We offer end-to-end bespoke product execution. This includes custom high-density silicone transfer logos, jacquard waistbands, laser-cut ventilation zones, custom-dyed matching drawcords, branded frosted zip bags, barcoded inventory tags, and customized packaging compliant with Amazon FBA and high-end retail distribution requirements.
Submit your tech pack, CAD drawing, or physical reference benchmark today. Our engineering and yarn specialists will review your specs, develop a tailored sampling schedule, and prepare a fully costed manufacturing plan within 24 hours.