In the rapidly consolidating international athleisure market, premium brands require manufacturing partners that transcend generic cut-and-sew operations. Our facility operates at the nexus of tubular circular knitting technology, micro-denier synthetic filament chemistry, and body-mapped compression ergonomics. As a verified premier Chinese seamless activewear manufacturer, we eliminate side-seam chafing, streamline fabric scrap from 18% down to under 2.5%, and program graduated muscle stabilization directly onto Italian-engineered Santoni cylinders.
Engineered from technical Polyamide 6.6 and Air-Covered Spandex blends. Fully customizable for private labels, gym studios, and luxury e-commerce brands.
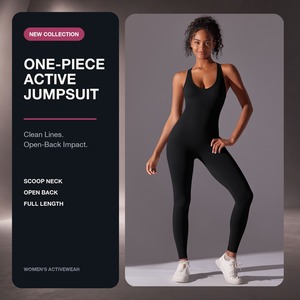
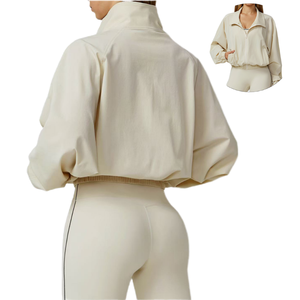
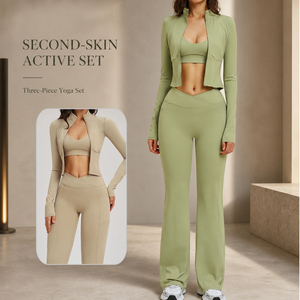
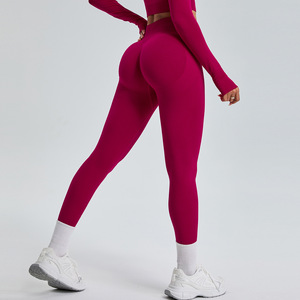
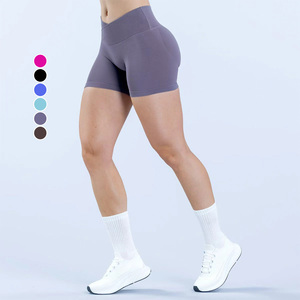
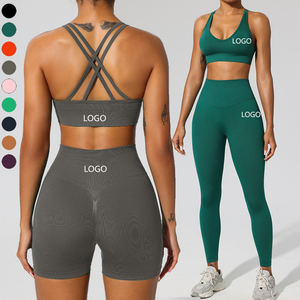
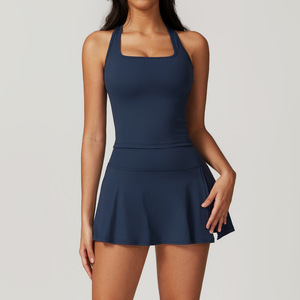
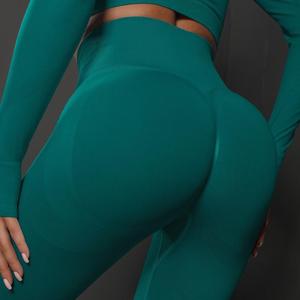
Vertical integration eliminates sub-tier subcontracting risks. From microfilament extrusion inspection to programmed electronic tensioners, every lot adheres to ISO 9001 and OEKO-TEX Standard 100 protocols.
Equipped with an advanced battery of gauge 28 and 32 Santoni electronic circular machines. We dynamically calibrate needle-selection systems, enabling real-time switching between rib knits, eyelet pointelle, honeycomb breathability zones, and high-tenacity tummy control panels in a continuous single-knitted tube.
Direct supply contracts with top-tier filament producers ensure access to virgin Polyamide 6.6 (Nylon 66), bio-based PA410, and GRS-certified post-consumer recycled chips. We deploy Air-Covering Spandex (ACY) technology to eliminate bare-elastane degradation, maintaining elasticity over 100+ industrial wash cycles.
Our dedicated R&D CAD engineering division translates raw vector art or reference competitor benchmarks directly into machine stitch binaries. Sample strike-offs, custom silicone gripper transfers, and reactive pantone lab dips are dispatched worldwide within one week.
Every knitted lot undergoes 100% greige-tube luminosity inspection for drop stitches, yarn snags, and denier variances. Finished garments undergo automated stretch recovery testing, tensile stitch validation, color crocking (dry/wet Grade 4.5), and spectrophotometric verification under D65 daylight.
Overcoming legacy mill bottlenecks, we support scaling DTC brands with low entry barriers: 1,000 pieces per style accommodates up to 2 size gradations and 3 colorway formulations. Reorder programs feature pre-dyed yarn inventories for compressed 20-day production cycles.
Complete branding integration: heat-transfer TPU reflective logos, jacquard woven underbust bands, recycled sugarcane polybags, FSC paper hangtags, and compliant GS1 barcode applications. We execute seamless DDP door-to-door forwarding across North America, Europe, Oceania, and GCC hubs.
A direct structural breakdown highlighting how seamless technology elevates garment ergonomics while dramatically lowering cost liabilities and fabric waste.
| Evaluation Parameter | Advanced Seamless Circular Knit | Conventional Cut-and-Sew Flatlock | Sourcing Impact Advantage |
|---|---|---|---|
| Structural Assembly | Continuous tubular knitting directly to contour; zero vertical side seams. | Flat fabric markers sliced into panels and joined via 4-needle 6-thread seams. | Eliminates Side Abrasion & Chafing |
| Targeted Compression | Programmed electronically stitch-by-stitch via denier changes within the cylinder. | Requires piecing multiple tension panels together with bulky sewn junctions. | Superior Anatomic Ergonomics |
| Raw Material Scrap Rate | < 2.5% scrap rate; yarn is consumed precisely to product perimeter dimensions. | 15% – 22% cutting offcuts discarded during pattern layout and nesting. | High ESG & Cost Efficiency |
| Tensile Seam Failure Risk | Virtually zero on torso and legs; stress is distributed across uniform knit loops. | Seam pop and thread breakage under maximum squat elongation stress. | Sub-0.2% Defect Return Rate |
| Texture & Pattern Iteration | Software-based jacquard file modification without cutting new steel pattern dies. | Requires re-grading patterns, knife cutting changes, and manual re-stitching. | 70% Shorter Design Iteration |
| Ideal Production Applications | Compression leggings, high-impact sports bras, unitards, and base-layers. | Loose woven running shells, heavy fleece tracksuits, cargo joggers. | Optimized Category Division |
To capture sustained market share, procurement executives must forecast yarn innovations, dynamic micro-climate regulations, and agile inventory structures.
Global regulatory pressure (such as EU Digital Product Passports) is pushing brands away from mechanical poly recycling toward depolymerized Polyamide 6 (Econyl/Q-Nova types) and castor-bean derived polyamides. Seamless activewear knitters that master bio-derived yarn tension control avoid microfiber shedding penalties while matching virgin tensile stretch and color fastness.
Forward-thinking athleisure procurement is shifting from surface chemical coatings to intrinsic yarn-embedded micro-encapsulated minerals. Utilizing Jade powder, graphene infusions, and bio-ceramic filaments, modern seamless knits regulate microclimates: dispersing body heat under high cardiovascular exertion and providing thermal reflection in rest states.
Consumers now reject flat monochrome workout sets in favor of tactile dimensionality. Circular knitting advancements enable true multi-color plating jacquard, shadow rib contours that lift and shape the glutes without cut-and-sewn ruching seams, and breathability panels that open when stretched, combining technical function with high visual appeal.
Long 6-month seasonal forecasts are obsolete. Market leaders now deploy lean, agile replenishment models: launching initial capsule collections with 500-unit runs per SKU, monitoring TikTok and Shopify conversion velocity, and utilizing pre-held greige tubes for automated reactive piece-dyeing in 14-day turnaround windows.
Traditional antibacterial top-finishes wash out after 20 laundry cycles, polluting water tables. The future belongs to permanent antimicrobial solutions: infusing silver or zinc ions directly into the polymer liquid melt prior to yarn extrusion. This ensures lifetime anti-odor performance without compromising hand-feel or fabric compliance.
The boundary between seamless circular knitting and luxury tailoring is merging. Advanced activewear blends circular-knitted core torsos with ultrasonic welded hem lines, laser-cut bonded ventilation, and frameless heat-bonded internal silicone support ribs, eliminating both seams and traditional elastic band bulk.
Clear, definitive answers addressing technical minimums, machine gauges, color fastness, shrinkage parameters, and private label execution.
Our standard manufacturing baseline is 1,000 pieces per style. Crucially for brand line-planning, this minimum can be divided across up to 2 size configurations (e.g., 500 S/M and 500 L/XL) and up to 3 custom colorway formulations. For bespoke jacquard development requiring dedicated cylinder recalibration, our technical team evaluates custom threshold tiers upon reviewing your initial tech pack.
We eliminate sheer degradation through three engineering controls: First, we knit on high-density Gauge 28 or 32 machines. Second, we deploy specialized double-covered yarn structures where fine multi-filament Nylon encapsulates the inner Spandex core. Third, our target fabric weights range between 280 to 350 GSM for leggings, ensuring full light-blocking opacity even at maximum 120% biaxial stretch.
Yes. Over 40% of our OEM accounts originate from physical benchmark samples. Our textile engineers perform optical de-knitting analysis to determine exact yarn denier, filament strand counts, elastane percentages, and loop densities. Within 5 working days, our CAD division replicates the stitch pattern into our machine programming system and knits a counter-sample for fit approval.
Proto sampling for existing machine programs takes 5 to 7 business days. Complex custom jacquards and bespoke pantone laboratory dips require 7 to 10 days. Once the pre-production sample (PPS) and packaging specs are signed off, bulk cylindrical production, dyehouse lotting, quality inspection, and packaging are completed within 28 to 35 calendar days.
We execute high-temperature overflow jet dyeing utilizing Datacolor spectrophotometric recipe controls, ensuring strict Delta-E values ≤ 0.8 compared to approved Pantone swatches. For dimensional stability, finished tubular knits undergo continuous tensionless hot-air relaxation drying and heat setting, capping residual laundry shrinkage below 3% in both warp and weft dimensions.
We offer turnkey branding integration: high-elasticity silicone logos, reflective 3M heat transfers, knitted-in jacquard waistband brand lettering, laser-cut custom ventilation patterns, woven satin or recycled damask care labels, branded hangtags, and custom EVA biodegradable ziplock packaging bags with pre-printed logistics barcodes.